

Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
Full Cutting Method Range — One manufacturer covering both knife and laser platforms lets you match the process to the material instead of forcing a single technology across every job.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
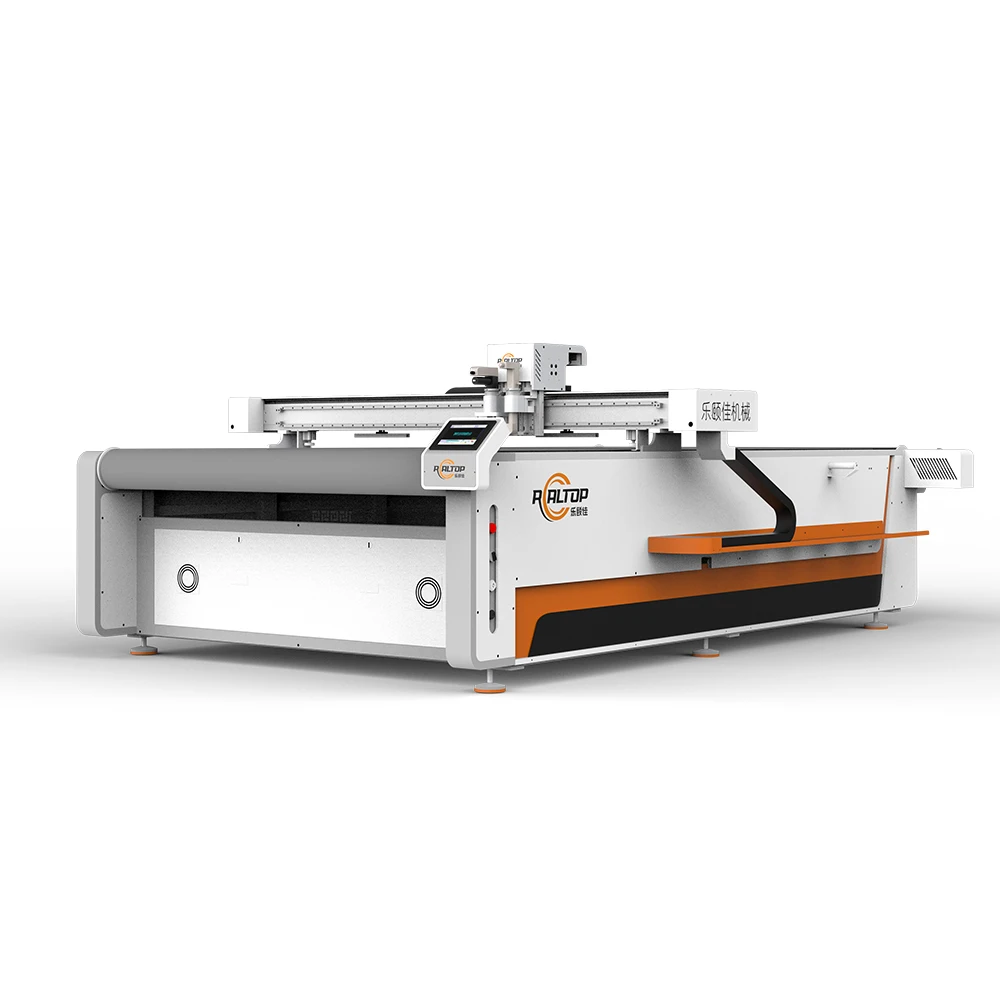
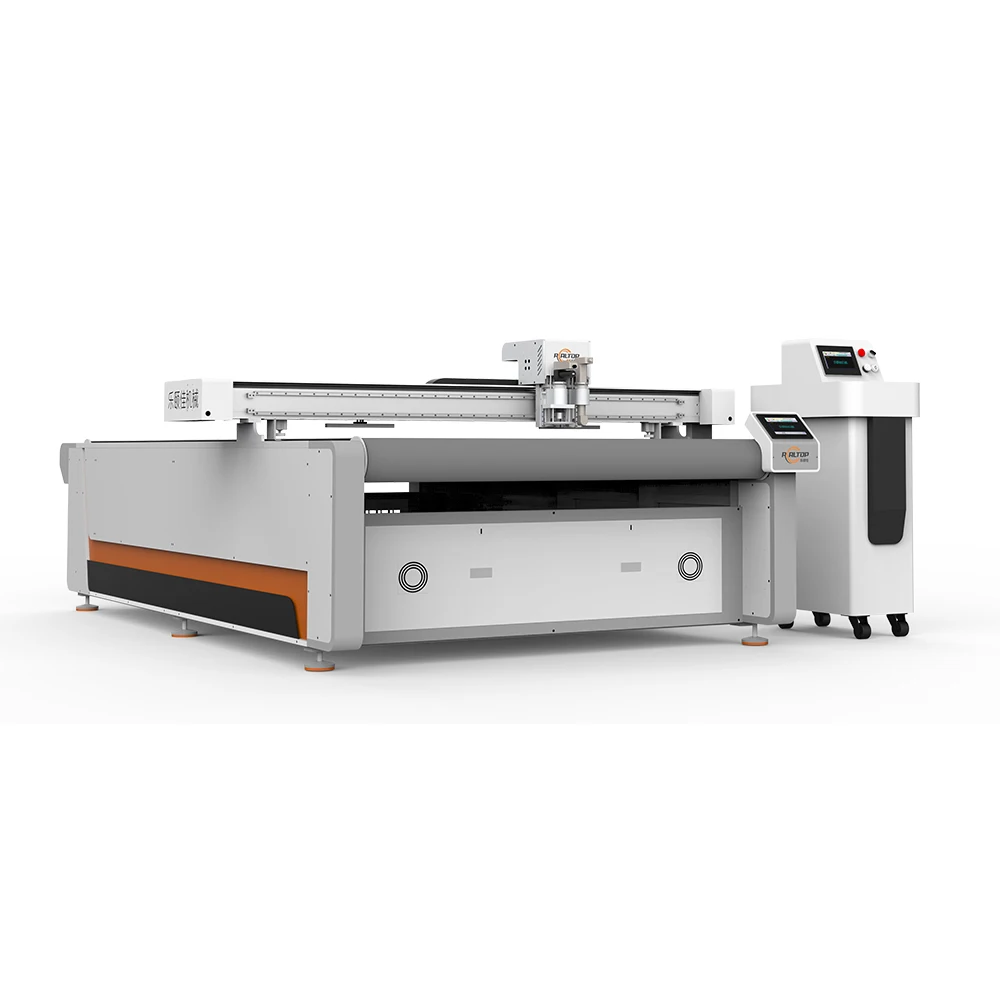
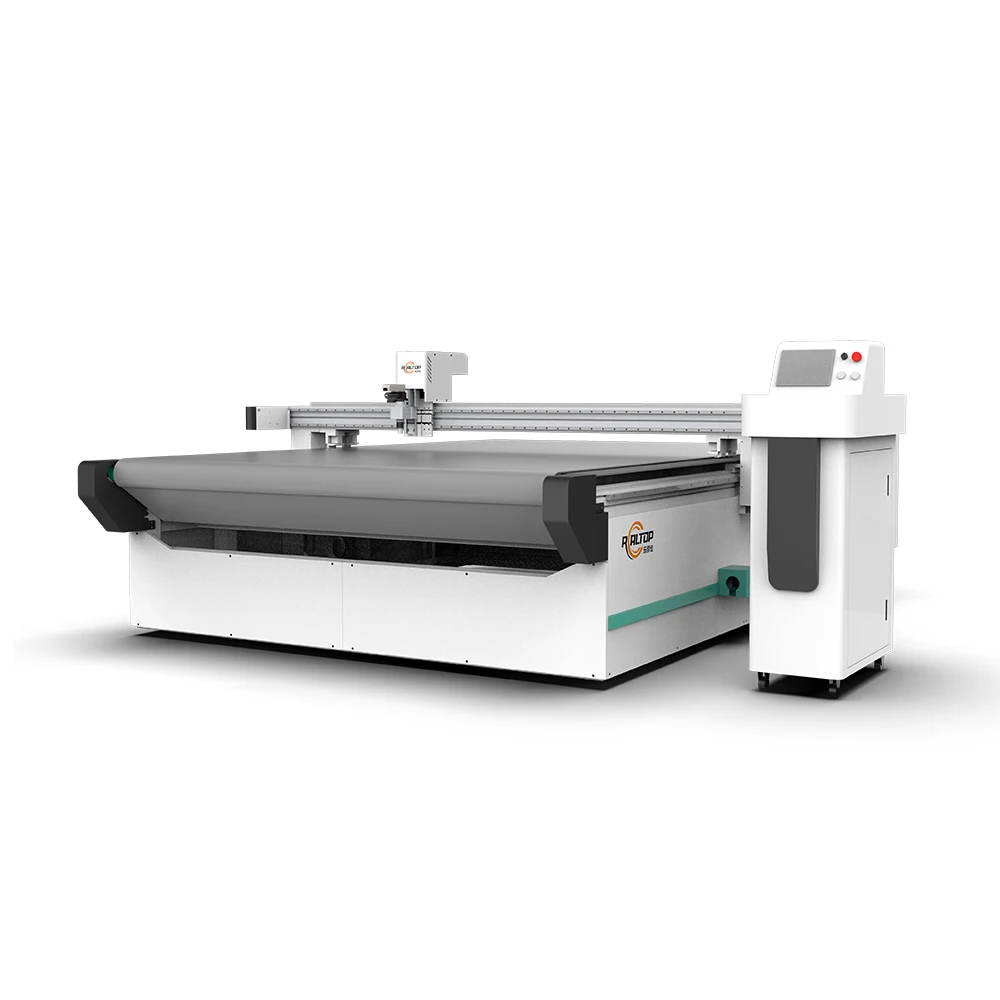
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500mm |
| Machine Size | 3450×2300×1250mm |
| Rated Power | 9kW |
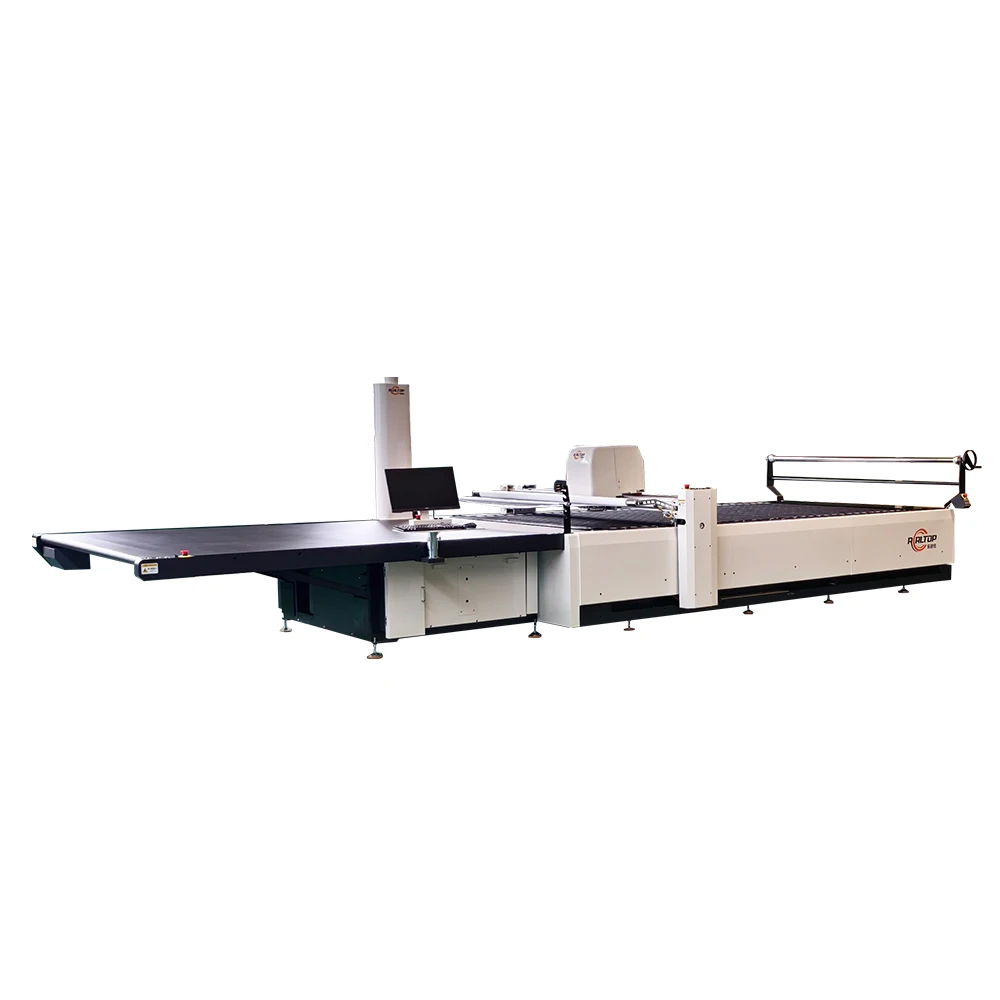
| Table Type | Flat working table or auto-feeding conveyor (configurable) |
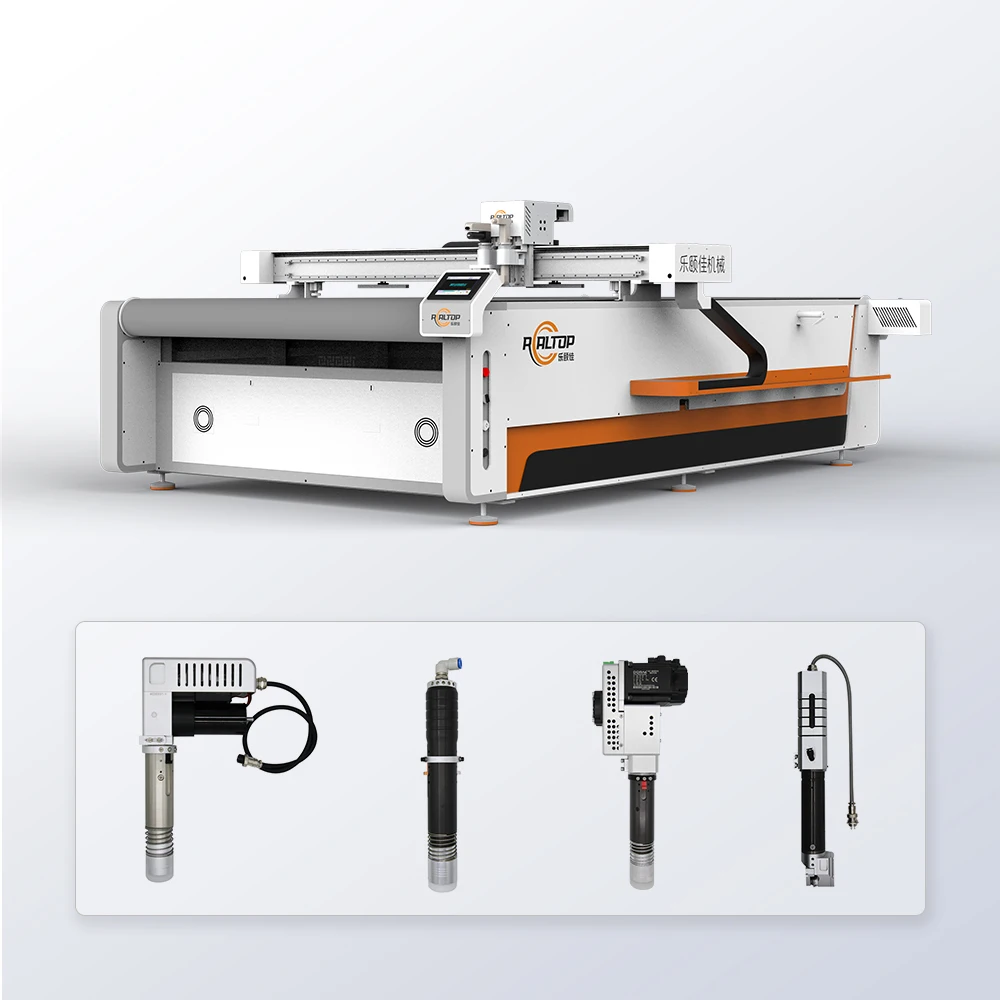
| Tool Head Options | Swiss imported knife, oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V-cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Translational Velocity | 800–2000mm/s |
| Cutting Speed | 200–800mm/s (basis not stated in source — confirm material and thickness) |
| Cutting Thickness | Up to 100mm depending on material |
| Repeated Accuracy | ≤0.1mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, imported ball screw |
| Servo Motor Options | Delta (China) or Panasonic (Japan) |
| Vacuum Pump | 7.5kW |
| Vacuum Table | Magnesium-aluminum alloy with PVDF powder spraying and anodic oxidation |
| Conveyor Belt | Germany imported |
| Linear Rail | Taiwan Hiwin |
| Control Panel | Touch screen with multi-language support |
| Instruction System | HP-GL compatible |
| File Format Support | PLT, DXF, AI |
| Visual Positioning | Small CCD mark point, panoramic camera, or projection positioning (optional) |
| Voltage | 380V±10% |
| Safety Devices | Infrared sensors, beam anti-collision, emergency stop with in-situ resume |
| Standards | CE referenced in documentation |
Application Suitability
| Application | Material or Output |
|---|---|
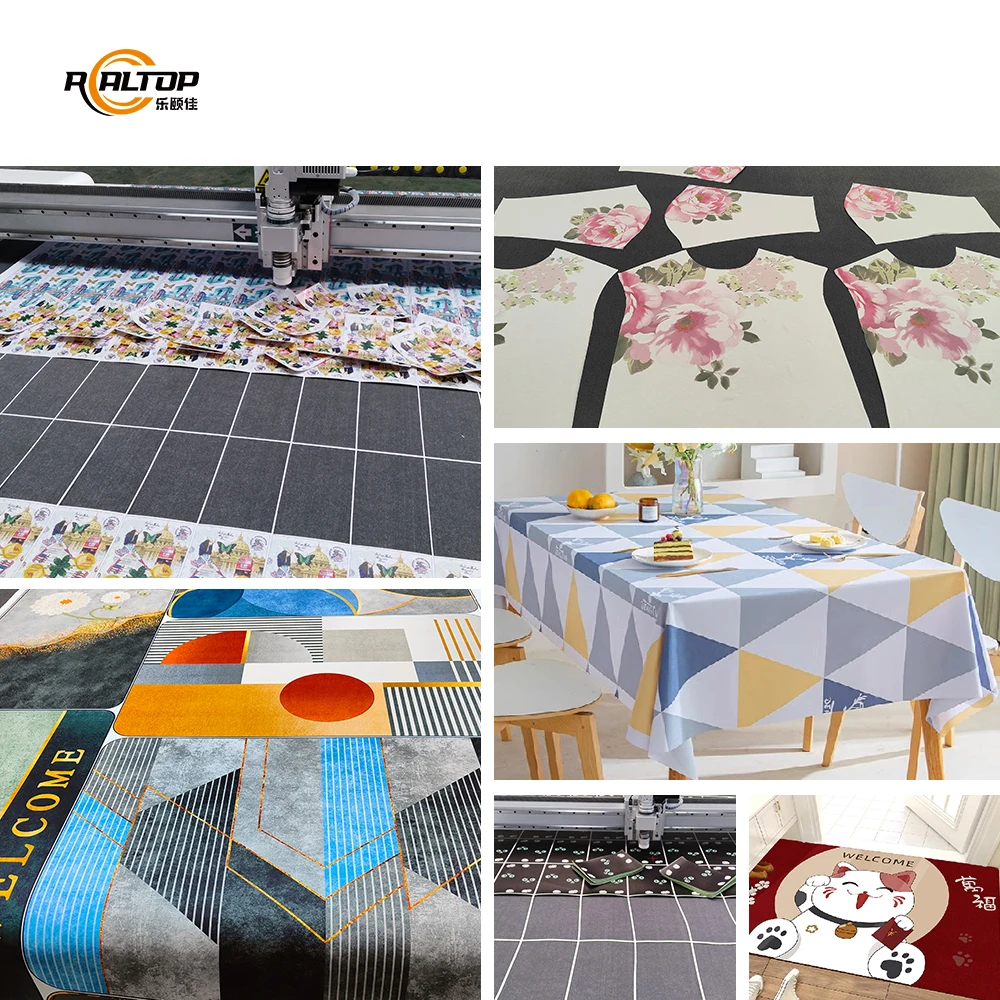
| Garment and footwear production | Woven fabric, knit textile, leather, shoe upper material, luggage material |
| Automotive interior trimming | Sponge composite leather, foam, gasket material, PU, EVA |
| Soft home furnishing | Carpet, sofa fabric, non-woven fabric, sponge |
| Packaging and carton sample making | Corrugated cardboard, cardboard, plastic box, sticker, film |
| Sealing and gasket fabrication | Rubber, silicon, PTFE, ETFE, fiberglass |
| Composite material fabrication | Carbon fiber, PVC, PP, PE, XPE, foam board |
Why Buyers Still Get the Wrong CNC Oscillating Knife Cutting Machine
The spec sheet looked correct until the material hit the table.
Every year I see workshops take delivery of a CNC oscillating knife cutting machine that is dimensionally perfect for their floor space but completely wrong for the stock they actually run. The working area matched the nest layout, the vacuum pump seemed adequate on paper, and the price was right. Then the first roll of coated composite arrived and the blade dragged, the vacuum lost grip on small cut pieces, and the daily throughput dropped to a fraction of what the brochure implied [NEED_CITE: common misconfiguration issues in digital cutting procurement]. The gap between a machine’s rated envelope and its real cutting behaviour on a specific material is where most procurement mistakes hide.
Mapping the Equipment Families to Your Material
The RT-D2516 and RT-S2516 sit within a broader catalogue that spans knife cutting and laser cutting from one production floor. Buyers surveying options on lyjcut.com can compare the oscillating knife approach for thick composites and layered textiles against CO2 or fiber laser routes for acrylic, wood, and sheet metal. This side-by-side visibility matters because the cutting method should follow the material, not the other way around. A garment producer cutting coated technical fabric needs clean mechanical edges that a laser would melt and seal differently. An automotive gasket shop cutting PTFE sheets needs blade pressure that a drag knife cannot deliver. The CNC oscillating knife cutting machine range here covers those mechanical cutting jobs, while the laser families handle the thermal processes.
Configuring the Table and Feed for Your Volume
Flat working tables suit batch production where an operator lays each sheet by hand and inspects the nest before cutting. Auto-feeding conveyor tables, fitted with the Germany-imported belt, serve roll goods and continuous textile runs where material flows through the cutting zone without manual repositioning. The choice between these two configurations depends on daily volume and material format more than on the machine frame itself. High-volume fabric producers cutting hundreds of meters per shift gain noticeably from the conveyor setup, while packaging sample makers switching between cardboard grades benefit from the flat table’s flexibility. The 7.5kW vacuum pump paired with the magnesium-aluminum alloy table holds workpieces in place during high-speed traversals, and the PVDF powder-sprayed surface resists the abrasion that corrugated and fiberglass stocks produce over time [NEED_CITE: vacuum table material selection for abrasive composites].
Reading the Specs That Actually Matter on the Floor
The 1600×2500mm working area fits standard textile roll widths and full hide leather layouts, which avoids the waste that comes from cutting material down to fit a smaller table. The Swiss imported knife, paired with options like the pneumatic knife and high-power vibrating knife, covers a thickness range up to 100mm — though actual depth depends heavily on material density and fibre structure, so sample cutting on the buyer’s own stock is the only reliable test. The Taiwan Hiwin linear rails and imported ball screws maintain the ≤0.1mm repeated accuracy across long cutting runs, which matters when nested garment pieces must align during sewing. The Delta or Panasonic servo motor choice affects serviceability in different export markets, since local technicians can source Delta parts more easily in Southeast Asia while Panasonic servos are preferred by some European importers.
What Happens When the Tool Head Does Not Fit the Job
Selecting a drag knife for a material that requires an oscillating knife produces crushed foam edges and frayed textile fibres that fail quality inspection. A circular knife on a stiff corrugated board sheet leaves incomplete cuts at corners because the blade cannot stop and change direction like a reciprocating head. I once visited a workshop where the operator had spent weeks adjusting feed rates to compensate for the wrong tool head, when a simple head swap would have solved the problem on day one. The vacuum zoning also plays a role here — small gasket parts lifted off the table during cutting because the adsorption zones were not matched to the nest layout, and the cut quality suffered as a result [NEED_CITE: vacuum zone configuration for small-part digital cutting]. These mismatches do not show up on a specification sheet, which is why running the buyer’s actual material before the order is confirmed remains the most reliable validation step.
Why Sourcing From This Catalogue Makes Sense
The design team and core factory cover both knife and laser cutting technologies under one roof, so a distributor can source a complete range from a single manufacturer rather than coordinating multiple suppliers. Tool head and table configurations are specified per material and production volume, not sold as a one-size package. CCD camera positioning — available as small mark-point, panoramic, or projection options — is confirmed against the buyer’s printed artwork before the machine ships. Software compatibility for PLT, DXF, and AI files is verified with the buyer’s existing workflow during the inquiry stage. Voltage, control language, and plug standards are documented and confirmed before production begins, which eliminates the shipment surprises that cost importers weeks of downtime [NEED_CITE: voltage and frequency standards by export market].
Documentation & Verification
- Machine specification sheet listing tool head and table configuration per material
- Electrical schematic with voltage and frequency confirmed for target market
- Sample cutting report produced on buyer’s own material before order
- Software licence and file format compatibility note for PLT, DXF, AI workflows
- Factory test record covering repeated accuracy and vacuum hold performance
- Packing photographs documenting machine condition before crating
Installation, Commissioning & Support
- 3450×2300mm footprint requires clear floor space plus operator access on three sides
- 9kW rated power plus 7.5kW vacuum pump need dedicated circuit at 380V±10%
- Machine arrives partially assembled; gantry and table leveling completed on site
- Touch screen control panel configured for local language before commissioning
- Tool head calibration performed across full 1600×2500mm working area during setup
- Wear parts list covers knife blades, vacuum seals, and conveyor belt segments
What We Need From You to Move Forward
Send the material type, maximum thickness, sheet or roll dimensions, and expected daily volume so the correct tool head and table configuration can be matched. Confirm the local voltage and frequency at your facility, along with the preferred control panel language, to avoid any post-shipment adjustments. If your existing software workflow uses a specific nesting file format, share a sample file so compatibility is verified before the order is placed.
Frequently Asked Questions
Q: How do I decide between oscillating knife and laser cutting for my material?
A: Oscillating knife suits fabrics, foams, gaskets, and composites where a clean mechanical cut without heat-affected edges is required. Laser cutting works for acrylic, wood, and certain textiles where edge sealing is beneficial. The choice depends on material composition, thickness, and the edge finish your downstream process demands.
Q: Which tool head should I specify for my material thickness?
A: Thin woven fabrics typically use a standard oscillating knife, while thicker foams and composites need the high-power vibrating knife or pneumatic knife for adequate stroke and pressure. Stiffer materials like corrugated board may require the creasing wheel combined with a cutting tool. Sample cutting on your actual stock confirms the correct selection.
Q: Should I choose a flat table or auto-feeding conveyor?
A: Flat tables suit batch production with varied materials and frequent sheet changes. Auto-feeding conveyors with the Germany-imported belt serve continuous roll-fed operations where material flows through the cutting zone without manual repositioning. Your daily volume and material format determine which configuration supports efficient workflow.
Q: What does the CCD camera positioning actually handle?
A: The small CCD camera reads printed mark points for contour cutting on pre-printed fabrics and labels. The panoramic camera recognizes larger printed areas for full-pattern matching. Projection positioning overlays the nest layout onto the material for manual alignment. Each option suits different printed contour workflows.
Q: Can the voltage and control language be customized before shipment?
A: Yes. Voltage is configurable at 380V±10%, and the control panel supports multiple languages. Electrical schematics and plug standards are confirmed during the specification stage so the machine arrives ready for local power supply without additional transformer or rewiring work on site.










商品评价
There are no reviews yet.