

Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
Knife and laser technologies in-house — the RT-D2516/RT-S2516 lets garment buyers match oscillating knife cutting to multi-layer fabric runs or switch to laser for synthetic edge sealing, all sourced from the same production line.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
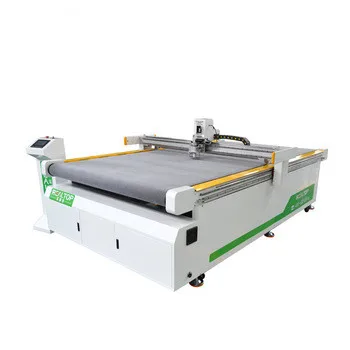
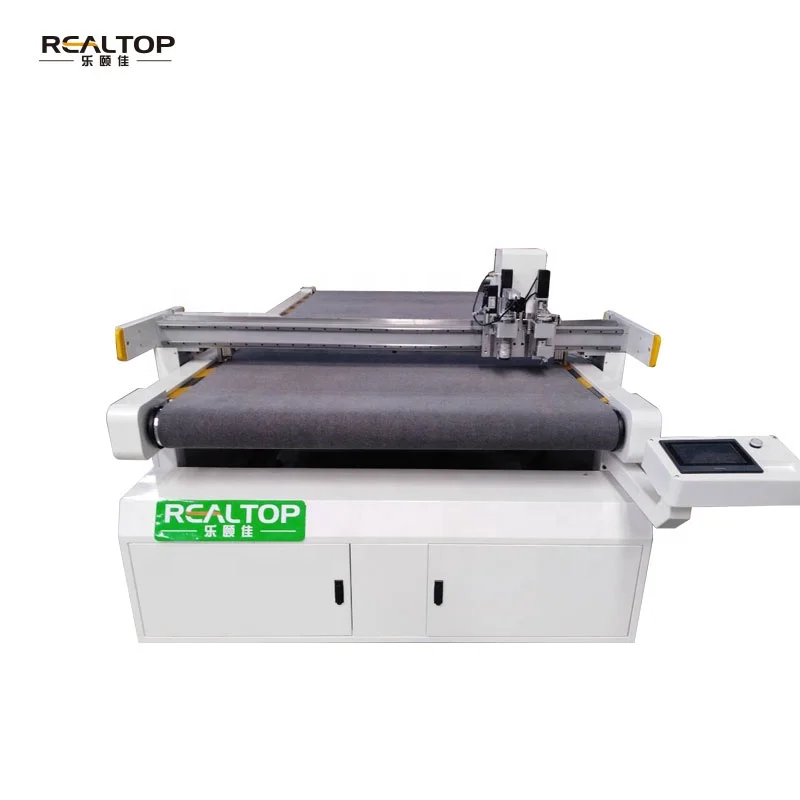
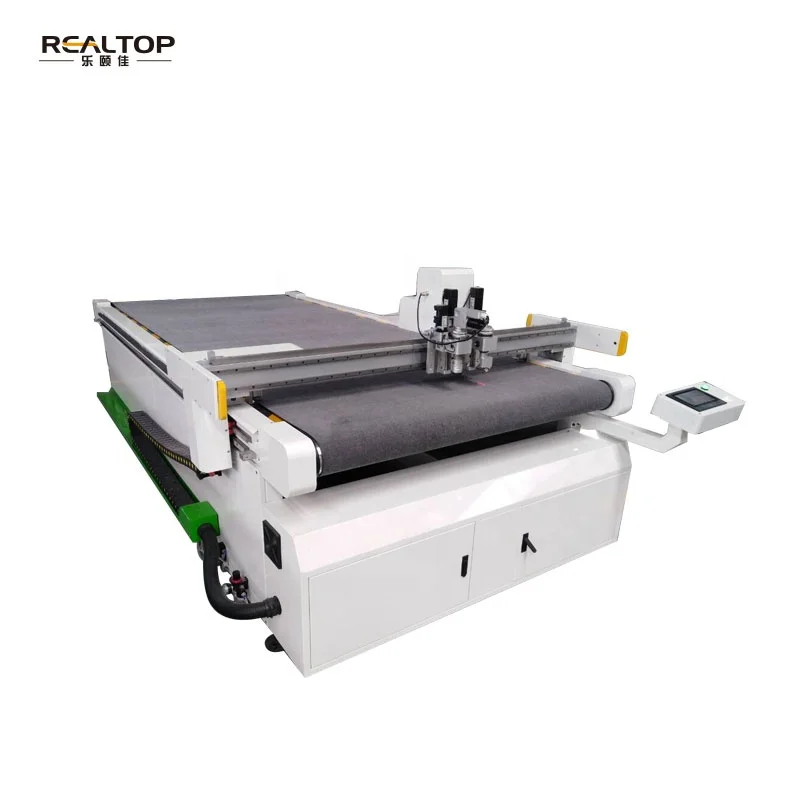
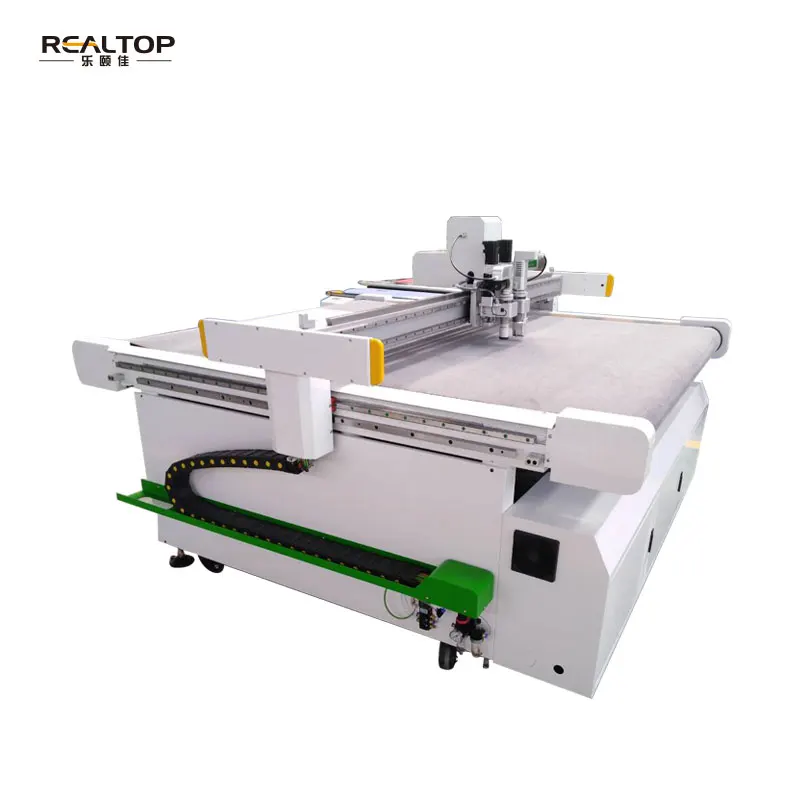
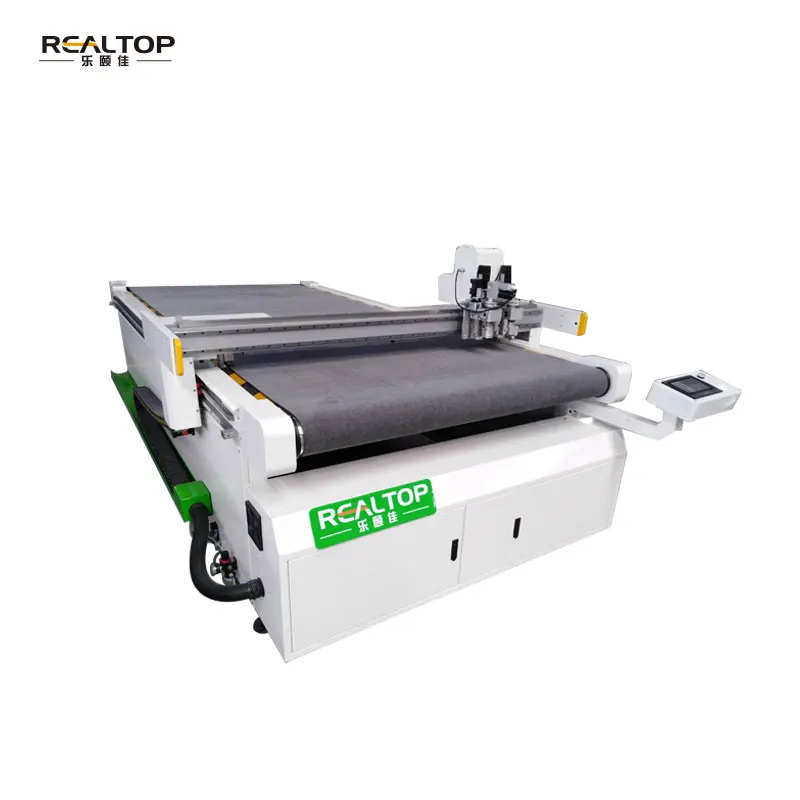
| Product Type | Multi-layer CNC Fabric Cutting Machine |
| Working Area | 1600×2500 mm |
| Machine Size | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Working Table | Flat working table with conveyor belt and vacuum table |
| Multifunctional Head | Swiss imported knife with vibration full cutting, vibration half cutting and cursor location function |
| Safety Device | Infrared sensors |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw (imported) |
| Servo Motor | Japanese Yaskawa |
| Instruction System | HP-GL compatible format |
| Voltage | 380V±10% |
| Conveyor Belt | Germany imported |
| Linear Rail | Taiwan Hiwin |
| Vacuum Pump | 7.5 kW |
| Auto Feeding | Yes |
| Key Features | Infrared safety sensors, auto-feeding conveyor, multi-tool head capability |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and suit cutting | Woven, knitted and layered cotton, polyester, wool blends |
| Leather goods and footwear | Natural leather, synthetic PU, sponge composite leather |
| Technical textile processing | PVC, soft glass, silicon sheets, rubber gasket stock |
| Flexible composite cutting | Laminated fabrics, coated textiles, foam-backed materials |
| Automotive interior trimming | Upholstery fabric, headliner material, carpet layers |
What Layer Count and Coating Type Really Mean for Your Multi-layer Fabric CNC Cutting Machine
A cutting speed figure on a brochure tells you nothing until you know which material and how many plies are stacked under the knife.
I once watched a garment workshop run a polyester stack smoothly on a flatbed cutter, only to switch to a TPU-coated composite the next week and see the blade stall, edges melt, and throughput drop sharply. The machine had not changed; the material had. Oscillating knife frequency, blade geometry and vacuum hold-down all behave differently once coatings, foams or adhesive interliners enter the stack. Buyers who skip a sample cut on their own lay-up often discover the mismatch only after the machine lands on their floor [NEED_CITE: material-dependent cutting behaviour in multi-layer textile processing].
Matching Knife Technology to Fabric Construction
A Multi-layer Fabric CNC Cutting Machine with a Swiss imported oscillating head handles woven and knitted layers by vibrating the blade at high frequency, shearing fibres cleanly instead of dragging them. This matters most when plies shift during the cut: the vibration keeps the blade travelling through the stack rather than pulling the top layers sideways. Half-cutting capability adds kiss-cut scoring for appliqué or pattern marking without penetrating the full lay-up, which is useful in suit canvassing where internal structure must remain intact.
Laser versus Knife Across the Full Catalogue
Within the complete cutting equipment range, the choice between knife and laser comes down to edge behaviour. Laser heat seals synthetic fibres as it cuts, preventing fraying on polyester sportswear and technical textiles, but it leaves a hard, burnt edge on natural fibres and melts thermoplastic coatings. Oscillating knife leaves a soft, clean edge suitable for tailoring and leather goods. Browsing the full catalogue lets a buyer compare both methods against the same material spec before committing to one platform [NEED_CITE: edge quality comparison between laser and knife cutting on coated textiles].
Reading the Specs Beyond the Working Area
The 1600×2500 mm bed accommodates standard garment marker widths, but the real constraint is vacuum zoning paired with the 7.5 kW pump. If zoning is too coarse, small pattern pieces near the table edge lose suction and lift mid-cut. Yaskawa servo drives on Taiwan Hiwin linear rails hold repeated accuracy to ≤0.1 mm, which keeps notch positions aligned across a full lay-up — critical when collar and cuff pieces must match across dozens of plies. HP-GL compatibility means the system accepts nesting files from common garment CAD packages without an extra conversion step.
The Cost of Choosing the Wrong Tool Head
Specifying a drag knife on a thick foam-backed composite may seem cheaper until the blade deflects through the stack, leaving the bottom plies uncut. Similarly, running a single-zone vacuum table on small gasket patterns causes parts to drift, producing scrap rather than finished pieces. These mismatches rarely show up in a factory acceptance test because the vendor runs a standard demo material. The buyer only sees the problem during their first real production shift [NEED_CITE: vacuum zoning impact on small-part cutting accuracy].
Why Source This Cutter from Realtop
The design team covers both knife and laser platforms, so a buyer can evaluate oscillating knife for suit fabrics and CO₂ laser for acrylic signage templates in a single consultation. Sample cutting runs on the buyer’s own material and layer count before order confirmation, eliminating guesswork. Voltage, plug type and control language are locked in at quotation stage — 380V±10% is standard, but other configurations are available for export markets. Factory test records include photographs of the actual machine and packing, not stock images. Spare parts lists cover blades, conveyor belt segments and vacuum seals so the first reorder does not become an emergency.
Documentation & Verification
- Machine specification sheet matching the agreed tool head and vacuum configuration
- Electrical schematic confirming voltage, frequency and plug type for the destination market
- Sample cutting report on buyer-supplied fabric with layer count and edge quality notes
- Factory test record with timestamped photographs before crating
- Software licence key and HP-GL file format compatibility note included in the shipping documents
Installation, Commissioning & Support
- 3450×2300×1250 mm footprint requires a level concrete floor with clearance for the conveyor feed and off-take side
- 9 kW main drive plus 7.5 kW vacuum pump need dedicated circuits; confirm breaker sizing before delivery
- Auto-feeding conveyor belt tension calibrated on-site after the machine is levelled
- First-article cut run on your fabric stack to verify knife frequency and vacuum zone mapping
- Operator training covers HP-GL file import, tool change and blade depth adjustment
- Spare oscillating blades and conveyor belt sections shipped with the initial order
Before You Send an Enquiry
Tell us the fabric type, ply count and maximum lay-up thickness you run daily. Confirm your workshop voltage, frequency and preferred control language. If you can send a sample roll of your most challenging composite material, we will run a test cut and return the pieces along with a configuration recommendation.
Frequently Asked Questions
Q: Knife or laser — which method fits my multi-layer fabric?
A: Oscillating knife suits natural fibres, woven stacks and leather where a clean, soft edge is needed. Laser seals synthetic fibres and prevents fraying on polyester or nylon but leaves a hardened edge on natural materials. We run both methods on your sample to compare edge quality and throughput before you choose.
Q: How do you specify the vacuum table for my pattern mix?
A: We review your nesting files to see the smallest part area. If pieces are small or irregular, the vacuum table is zoned so suction concentrates under each cluster, preventing lift during high-speed traversal. The 7.5 kW pump capacity is matched to total open zone area.
Q: Which file formats does the system accept?
A: The instruction system reads HP-GL compatible formats, covering output from most garment and footwear CAD nesting packages. If your workflow uses DXF or proprietary formats, we confirm import compatibility during the pre-order software check.
Q: Can voltage and control language be customised?
A: Standard configuration is 380V±10%, but motor wiring, transformer taps and plug type are adjusted to your local supply. Control interface language is set before shipment so operators see menus and error messages in their working language from day one.
Q: What happens during the sample cutting step?
A: You send a roll or sheet of your actual production material with the typical layer count. We run it on the configured head and table, then ship the cut pieces back with a report noting edge quality, cycle time observations and any blade or vacuum adjustments made.










商品评价
There are no reviews yet.