


Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
Configuration Matched to Material — A 400×600mm cutting area is only useful if the tool head, blade stroke, and vacuum zoning are specified for your exact substrate and thickness, which we verify with sample cutting before any order is confirmed.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | 1070PAS4 A1 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Max Working Area | 400mm × 600mm |
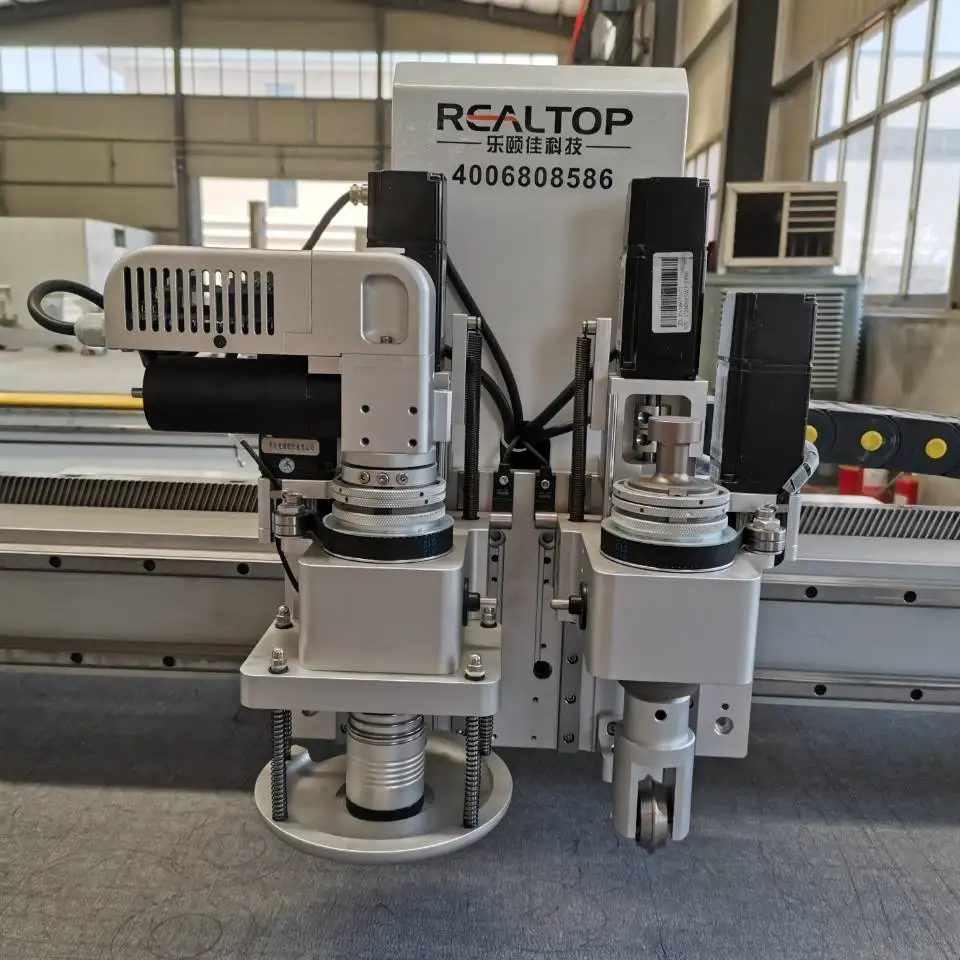
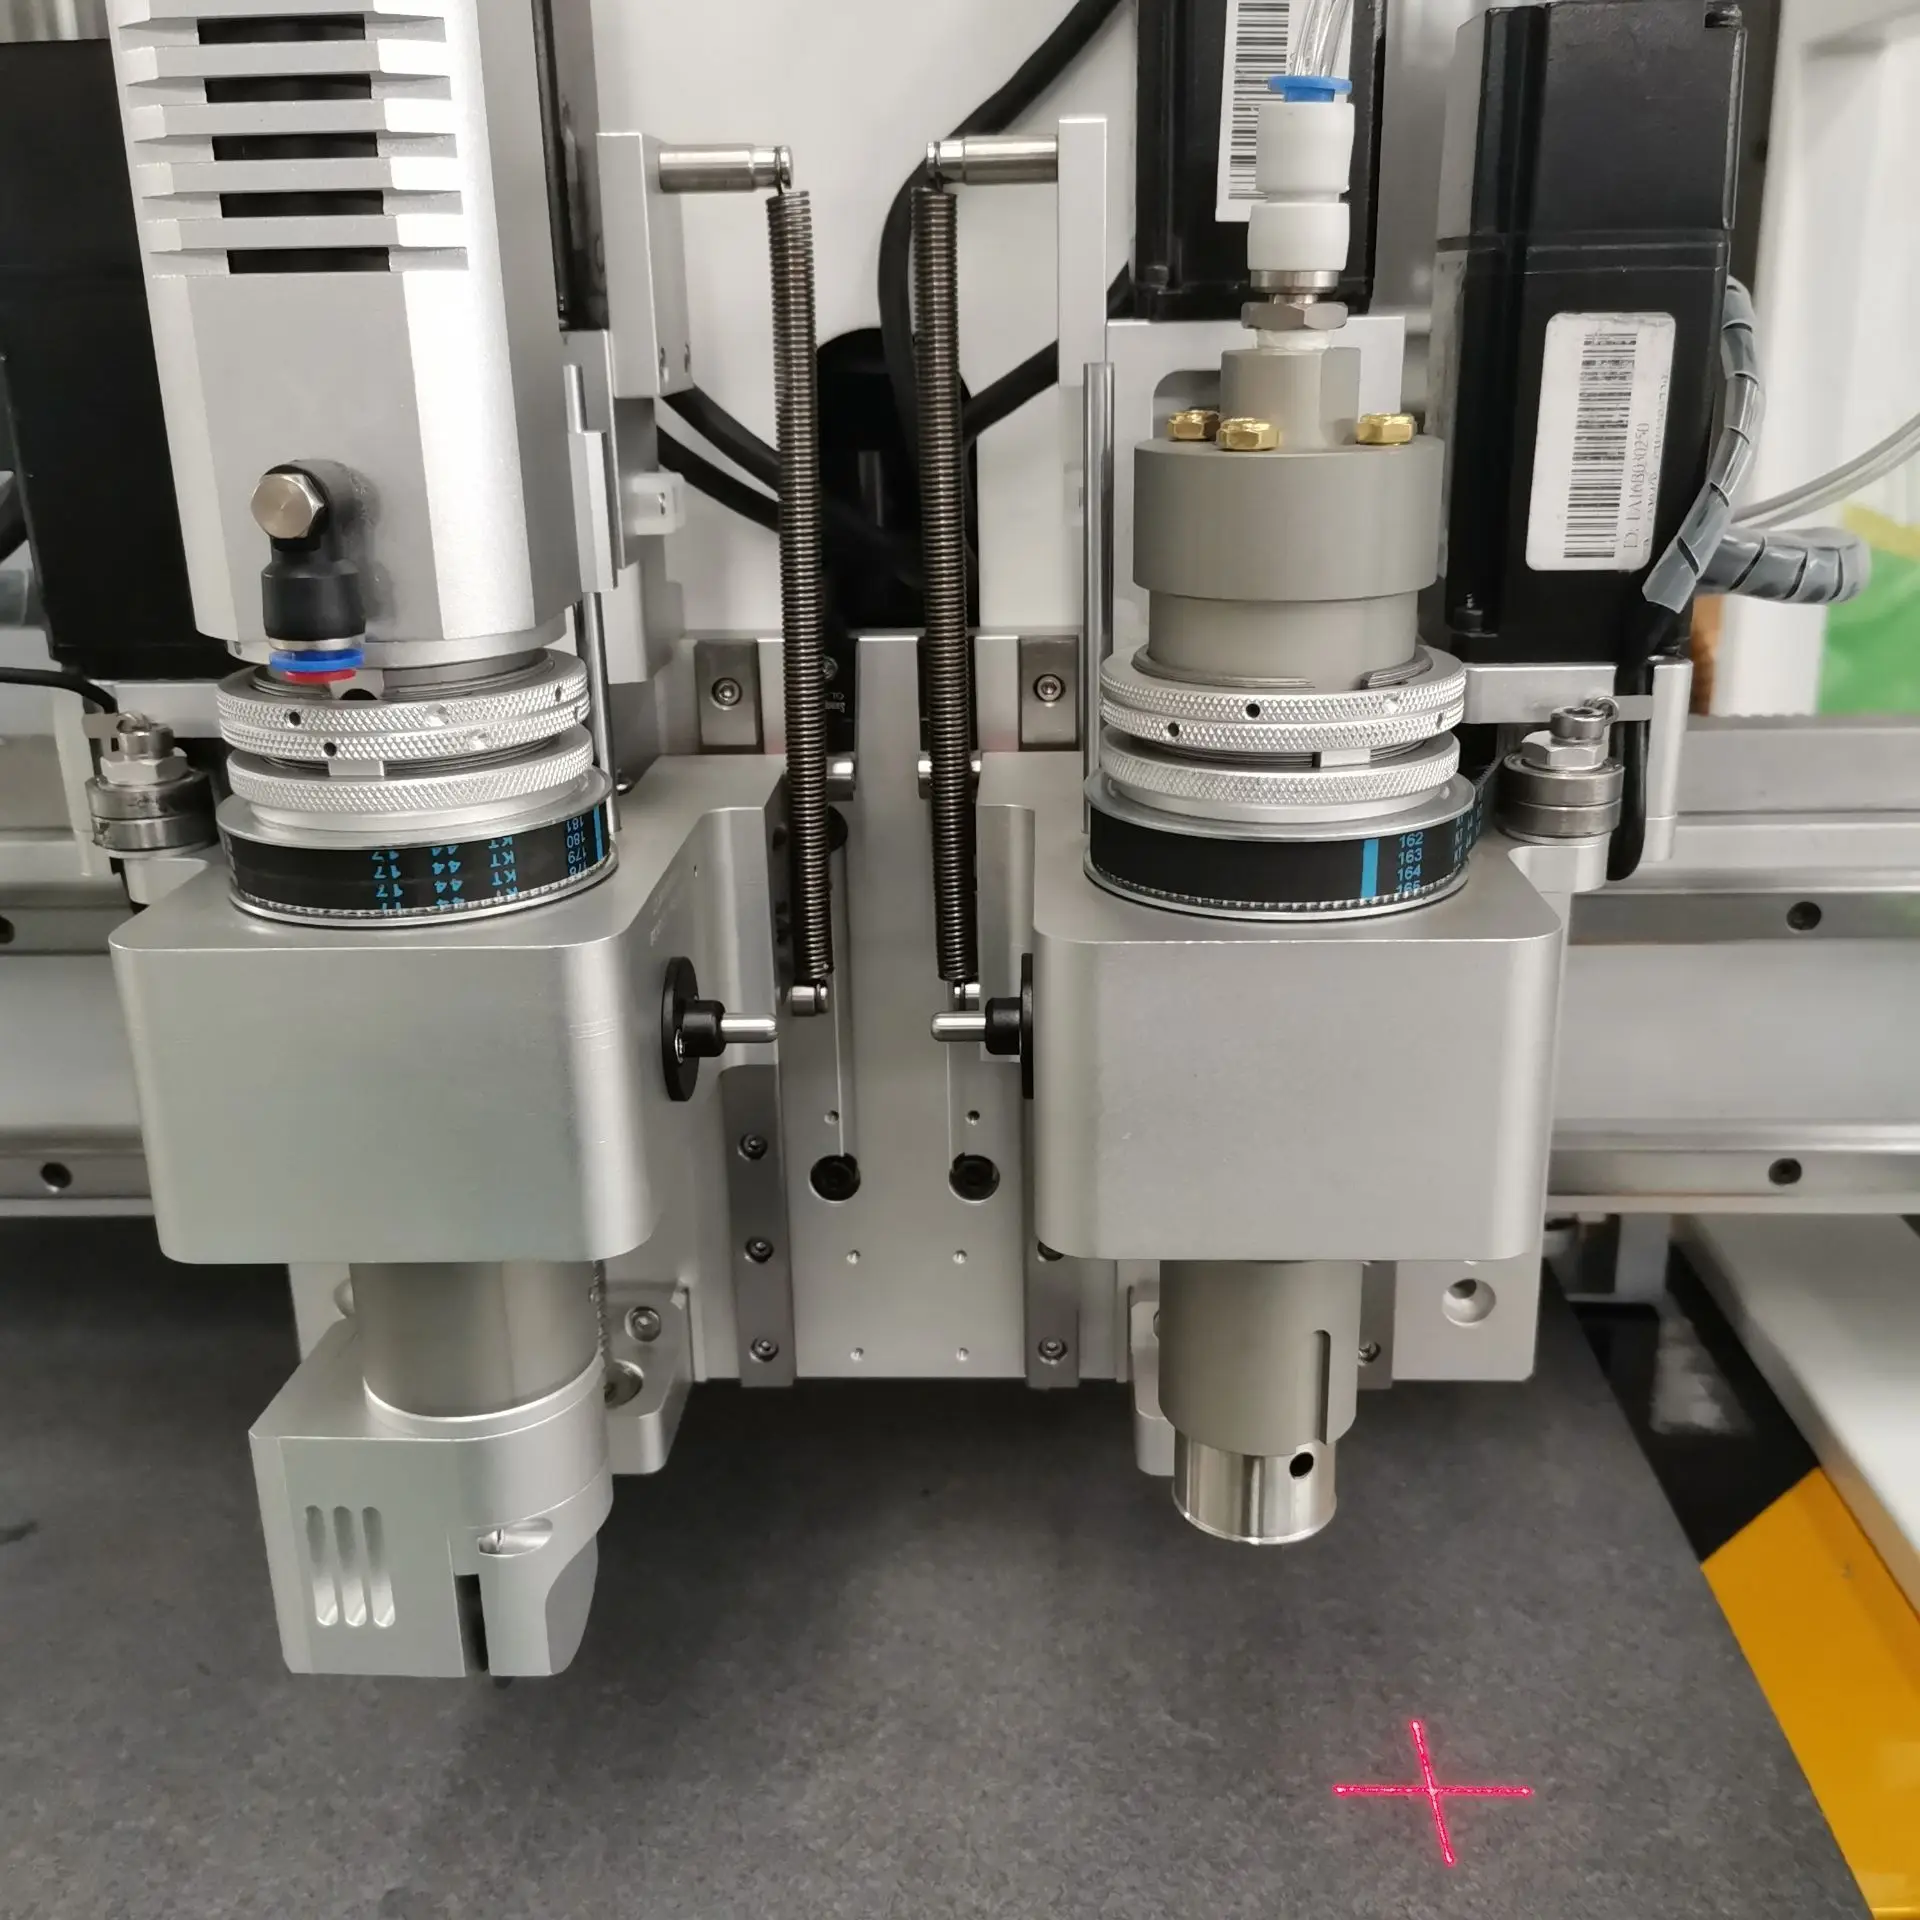
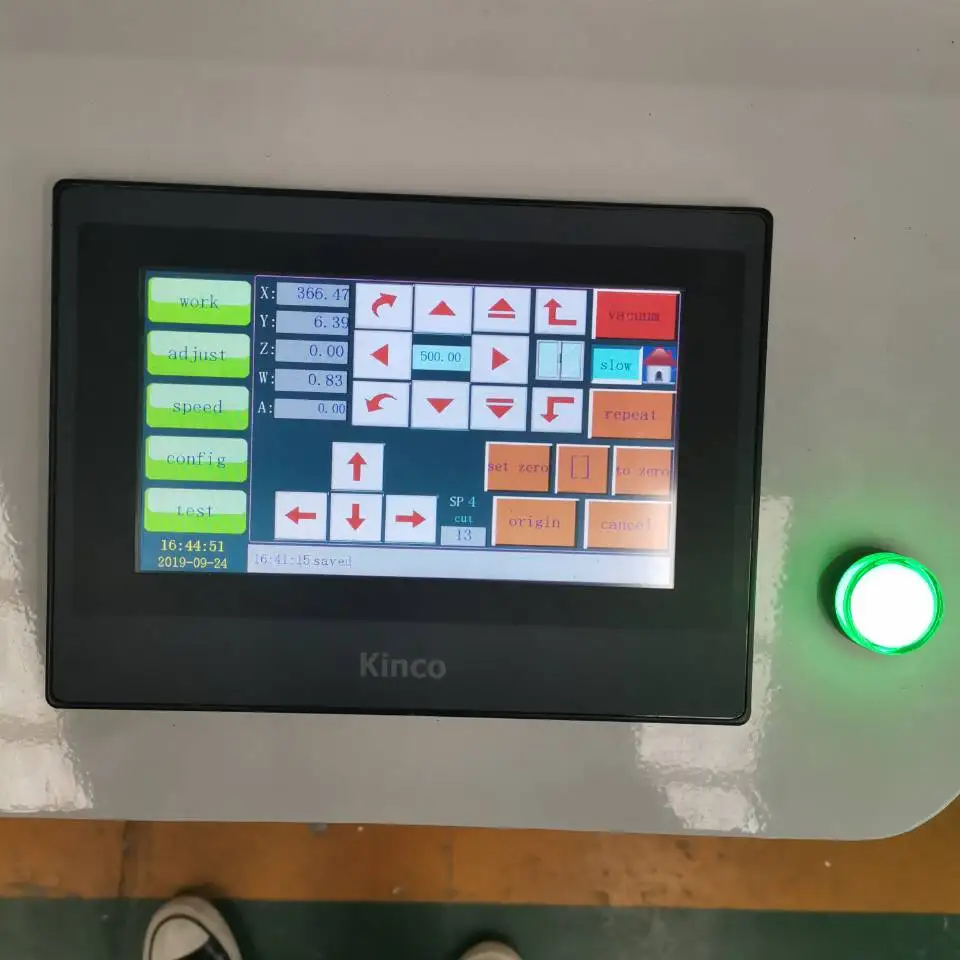
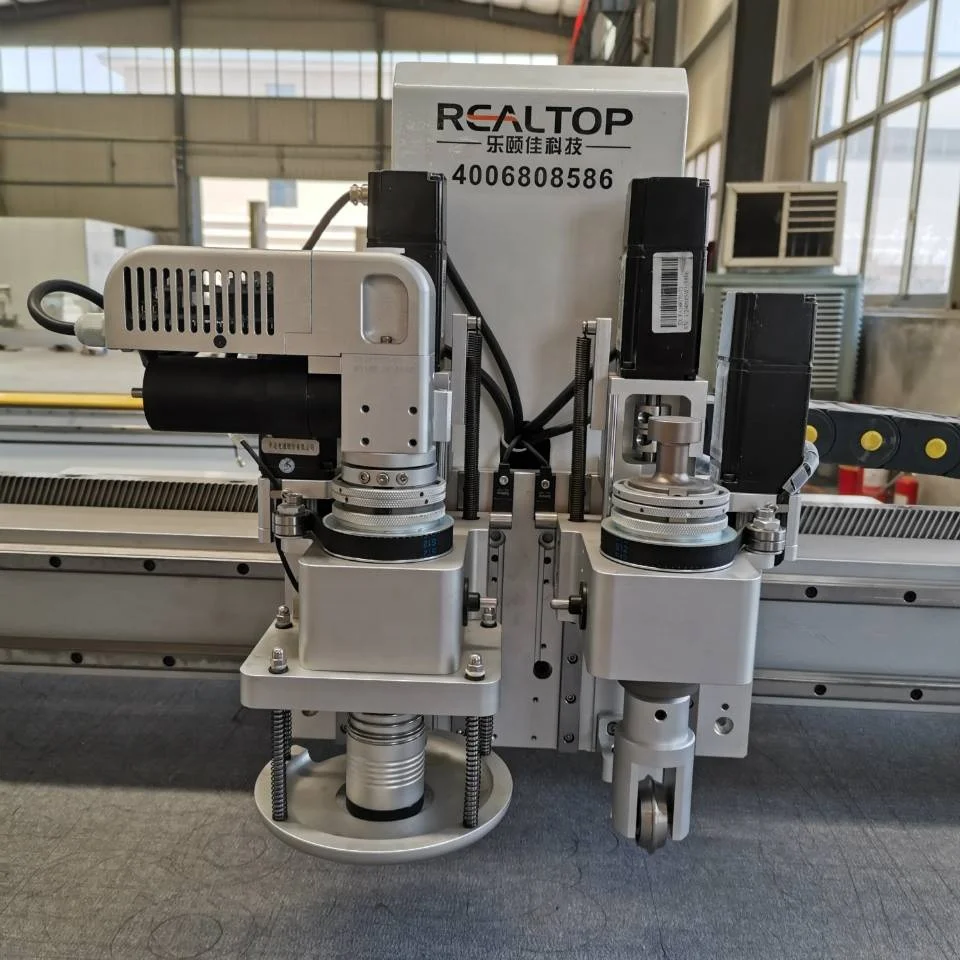
| Available Tool Group | Cutting Tool; Kiss-cutting Tool; Creasing Tool; CCD Camera; High Speed Oscillating Knife (RTT4060 Pro) |
| Max Cutting Speed | 1500mm/s (according to the material) |
| Cutting Thickness (RTT4060) | < 2mm |
| Cutting Thickness (RTT4060 Pro) | < 5mm |
| Positioning Accuracy | 0.05mm |
| Supported Profile Formats | DXF, OLT, PDF, AI |
| Transmission Method | Ethernet port |
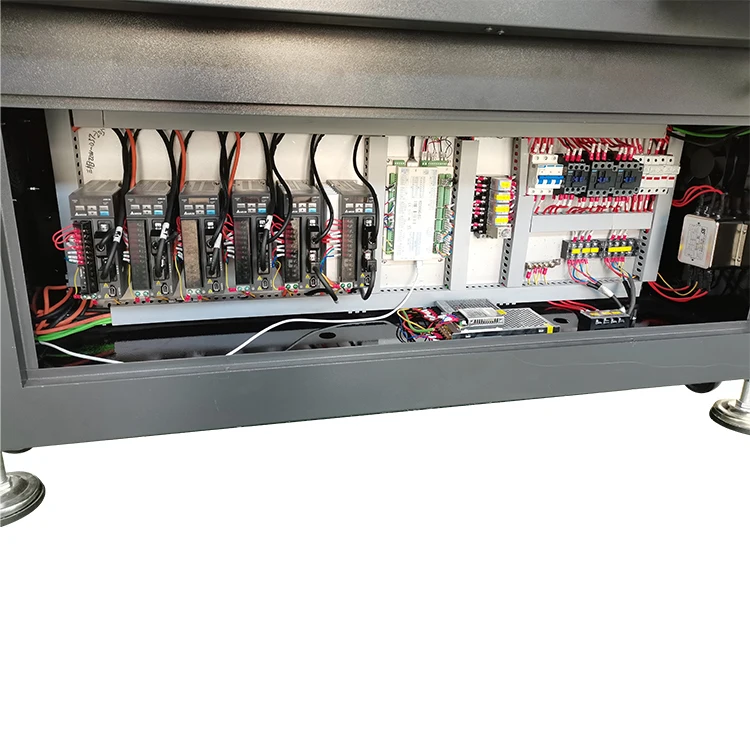
| Rated Power | 2.5kW |
| Assembly State | Fully assembled |
| Standards | CE declaration |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging sample making | Corrugated cardboard, greyboard, folding box board up to working thickness limit |
| Vinyl sticker and label production | Self-adhesive vinyl, reflective film, PVC sticker sheets with kiss-cutting |
| Advertising and signage material processing | Foam board, KT board, magnetic sheet, thin acrylic |
| Leather cutting | Genuine and synthetic leather for small-format accessories and prototypes |
| Carton prototyping | Single-face corrugated, E-flute and F-flute boards with creasing and cutting |
Why "Working Area Only" Specifications Fail on Sticker and Board Stock
The cutting area tells you what fits on the table — not whether the machine can actually process your material.
I have watched buyers specify a flatbed cutter based purely on bed dimensions, only to find the standard drag knife cannot penetrate 2mm reflective vinyl or that the oscillating stroke is too short for double-wall corrugated samples. A CNC oscillating knife cutting machine manufacturer should be asking about your material type, thickness range, and daily volume before quoting a configuration, because a mismatch between tool head and substrate produces ragged edges, incomplete cuts, or crushed flutes [NEED_CITE: material and tooling compatibility in digital flatbed cutting].
The 1070PAS4 A1 addresses this by offering distinct tool groups — including kiss-cutting for labels, creasing for cartons, and a high-speed oscillating knife on the Pro variant for denser stock — so the cutting method follows the material rather than the other way around.
Tool Head Selection Across Label, Board, and Leather Work
Each tool in the group serves a distinct production task. The kiss-cutting tool slices through the face film without damaging the release liner, which is essential for vinyl sticker runs where partial-depth accuracy determines whether labels peel cleanly. The creasing wheel scores fold lines on carton stock without severing the fibre, allowing packaging sample makers to produce functional folding prototypes. The oscillating knife, available on the Pro configuration, handles thicker and more fibrous materials that a drag knife would tear or stall on.
CCD Camera Contour Recognition for Printed Graphics
When cutting pre-printed sticker sheets or packaging mock-ups with registration marks, the CCD camera locates printed contours and adjusts the cut path accordingly. This matters at production speed, where even a small drift between the printed image and the cut line renders the sheet unusable. The system reads fiducial marks and compensates for stretch or skew introduced during printing [NEED_CITE: CCD registration accuracy in digital cutting systems]. Confirming mark style, contrast ratio, and placement with your artwork supplier before ordering ensures the camera can track reliably on your actual production files.
Reading the Specification Sheet for Real Cutting Capacity
Cutting thickness is the parameter that causes the most post-delivery disputes. The RTT4060 handles substrates under 2mm, while the RTT4060 Pro extends capacity to under 5mm — but these figures assume correct tool selection and appropriate blade geometry for the material in question. A 3mm foam board cuts differently from a 3mm leather sheet, even at the same nominal thickness. The 0.05mm positioning accuracy keeps cut paths tight against design geometry, which is particularly noticeable on small-format label work where a fraction of a millimetre determines whether a kiss-cut lifts cleanly. Ethernet transmission avoids the driver and cable issues common with USB-connected machines in workshop environments.
The Cost of Skipping Material Trials
When a buyer orders without sending actual production material for trial cutting, the first run on-site becomes the test — and any mismatch means wasted stock, delayed delivery, and eroded confidence. Reflective film that is 0.3mm thicker than the sample used during configuration can leave the drag knife unable to complete the cut, resulting in sheets that tear during weeding. Vacuum table zoning that is too coarse for small sticker parts allows edges to lift during high-speed passes, producing dimensional errors that only appear once production volume ramps up [NEED_CITE: vacuum hold-down requirements for small-format digital cutting].
Why Procurement Conversations Start with Your Material
The in-house design team covers both knife and laser cutting technologies, which means the recommendation is based on your substrate rather than limited to a single cutting method. Tool head and table configuration are specified per material and production volume, documented in the configuration list before order. Software compatibility — including DXF, OLT, PDF, and AI format import — is confirmed against your existing design workflow so there are no surprises at commissioning. Voltage, control language, and plug type are agreed in writing before production begins. Sample cutting on your own material is standard procedure, and the resulting report travels with the machine documentation.
Documentation & Verification
- Machine specification sheet listing confirmed tool heads, working area, and cutting thickness range for your material
- Electrical schematic with voltage and frequency matched to your facility supply before production
- Sample cutting report produced on your actual sticker, board, or leather stock with measured results
- Software licence and file format compatibility note confirming DXF, PDF, AI, or OLT workflow integration
- Factory test record showing positioning accuracy and cut quality verified prior to crating
Installation, Commissioning & Support
- 2.5kW rated power draw requires a dedicated single-phase circuit with correct breaker rating at your facility
- Fully assembled delivery means the 400×600mm unit can be positioned and connected without on-site mechanical assembly
- Ethernet port connection allows direct network integration with your existing design workstation
- First-run commissioning includes vacuum table zoning setup matched to your typical part size and geometry
- Operator training covers tool head changeover between cutting, kiss-cutting, and creasing for different jobs
- Spare parts list identifies blades, creasing wheels, and wear items with reorder codes for ongoing production
What to Include in Your Inquiry
Send the specific material types you process — whether self-adhesive vinyl, corrugated board grade, or leather weight — along with the maximum thickness and sheet size you run. Include your local voltage and frequency so the electrical system is built to match. If you use printed graphics with registration marks, share a sample file so CCD tracking can be validated before build.
Frequently Asked Questions
Q: How do I confirm the cutting thickness rating actually covers my material?
A: Thickness ratings assume correct tool selection and blade geometry for the specific substrate. A 3mm foam board and 3mm leather sheet behave differently under the same knife. We run sample cuts on your actual material and provide a measured cutting report before the order is finalized, so the thickness capability is verified on your stock, not just stated on a spec sheet.
Q: What marking system does the CCD camera need for reliable contour tracking?
A: The camera reads fiducial marks printed alongside your artwork. Contrast between the mark and the background, mark size, and placement relative to the cut boundary all affect tracking speed and accuracy. Share a sample of your printed sheet during the inquiry stage so we can confirm the CCD system locks onto your specific mark style at your intended production speed.
Q: Is the vacuum table zoning adequate for small sticker parts?
A: Small-format parts require fine vacuum zoning to prevent edge lift during high-speed passes. The table configuration is specified based on your typical part geometry and size range. If your production includes intricate label shapes, the zoning layout is adjusted accordingly and confirmed in the configuration list before manufacturing begins.
Q: Will my existing design files import without conversion issues?
A: The system accepts DXF, OLT, PDF, and AI profile formats. However, nesting workflow and layer naming conventions vary between software packages. We confirm file import and compatibility against a sample of your actual production files before order, and provide a written compatibility note with the documentation package so your design-to-cut workflow is uninterrupted.









商品评价
There are no reviews yet.