

Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
Complete Cutting Range — Buyers evaluate knife and laser cutting options across material types and production volumes rather than committing to a single forced method.
Technical Specifications
| Parameter | Value |
|---|---|
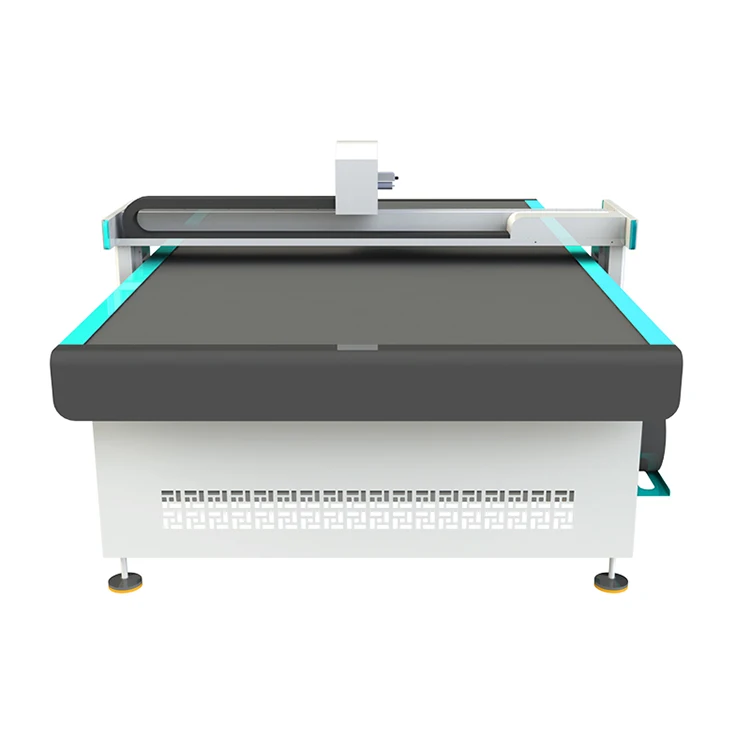
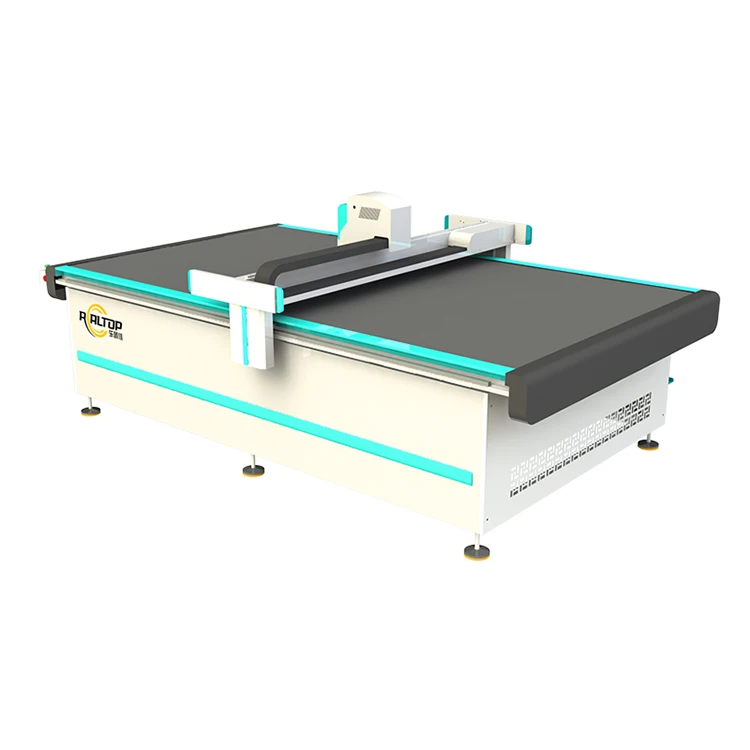
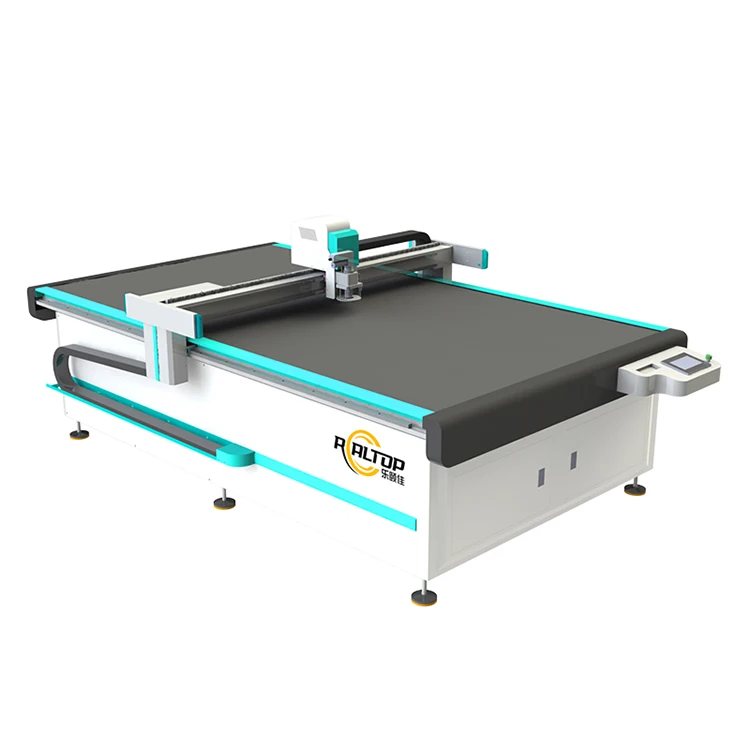
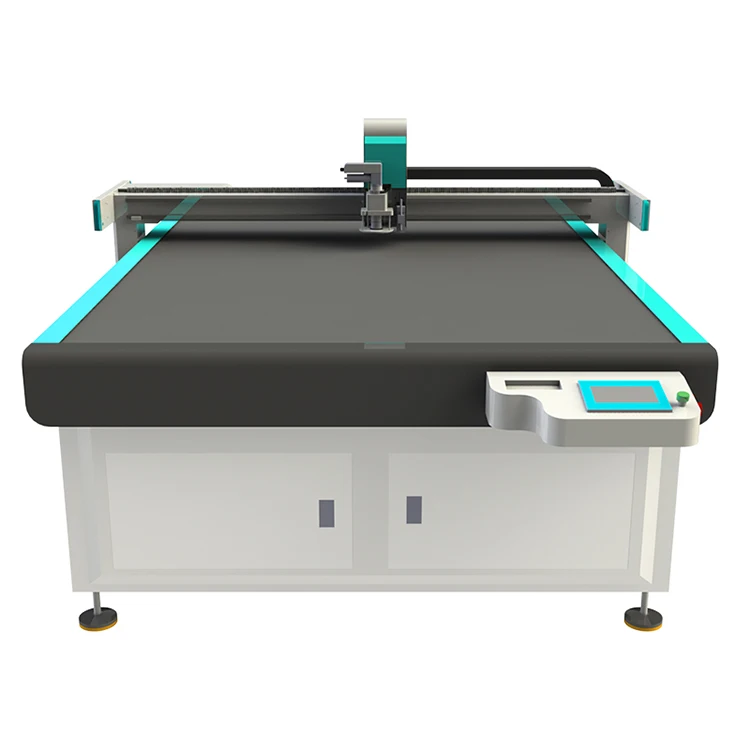
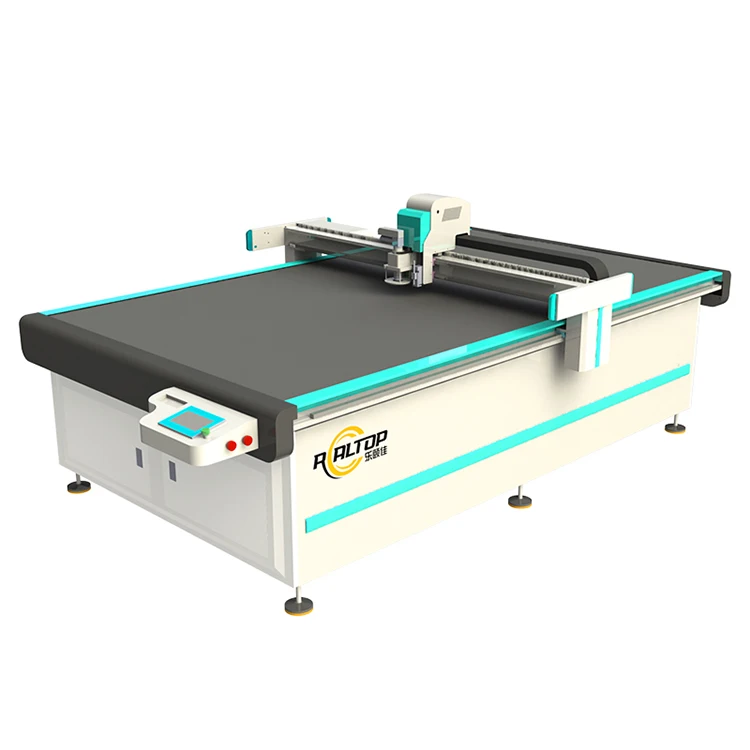
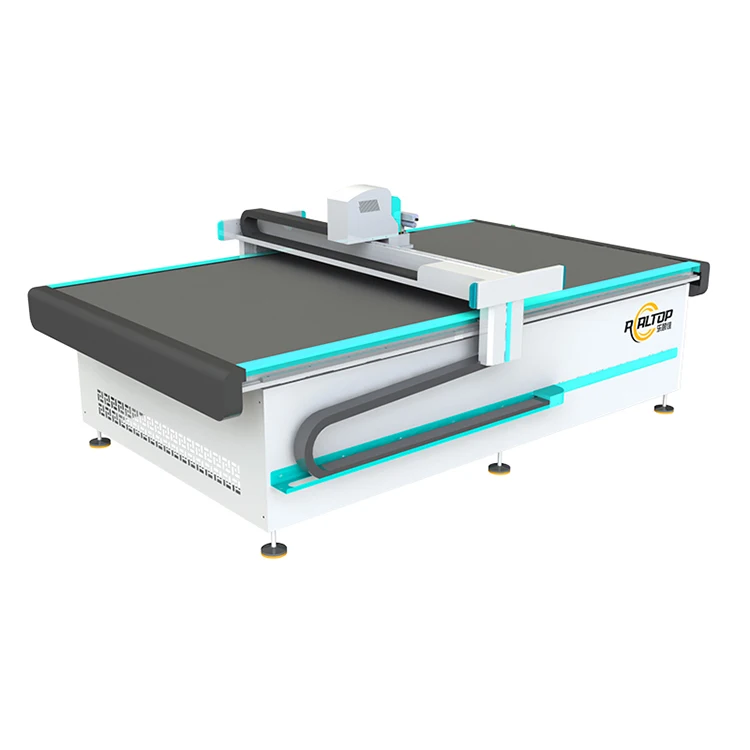
| Product Type | CNC Oscillating Knife Cutting Machine |
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Vacuum Pump | 7.5 kW |
| Table Type | Flat working table with vacuum |
| Tool Head | Swiss imported knife with vibration full cutting, vibration half cutting and cursor location |
| Servo Motor | Japanese Yaskawa digital servo |
| Guide Rail | Taiwan Hiwin linear guide |
| Conveyor Belt | Germany imported belt for auto feeding |
| Transmission System | Digital servo motor, linear guide, synchronous belt, imported ball screw |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s depending on material |
| Repeated Accuracy | ≤0.1 mm |
| Instruction System | HP-GL compatible format |
| Voltage | 380V ± 10% |
| Safety Device | Infrared sensors |
| Additional Features | Vacuum table, auto feeding system |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and footwear cutting | Layered fabric, clothing flexible material |
| Leather goods production | Natural and synthetic leather, sponge composite leather |
| Automotive interior components | Composite foam and fabric panels |
| Gasket and seal fabrication | PVC, soft glass, silicon, rubber |
| Packaging and sample making | Corrugated board, flexible packaging material |
Why the Wrong Tool Head Fails Before the First Shift Ends
A blade chosen for material A will crush, drag or fray material B the moment production starts.
I spent years walking factory floors across the Pearl River Delta watching operators fight machines that were sold on working area alone. The cutting head matched the demo sample perfectly, but the real production material was thicker, denser or more layered than the sample — and the edges came out ragged, compressed or delaminated. By the time the buyer realises the mismatch, the machine is already bolted to the floor [NEED_CITE: tool head and material compatibility in flexible cutting operations].
How Knife and Laser Divide the Catalogue
Buyers browsing the full range face a decision that no single machine answers. A CNC oscillating knife cutting machine manufacturer offering both knife and laser technology lets the buyer start with the material, not the machine. Fabric, foam and layered composites suit oscillating knife action because the blade moves vertically without generating heat, so synthetic fibres and adhesive layers stay intact through the cut.
When CO2 Laser Takes Over the Cut
Acrylic, wood veneer and thin textiles often perform better under a CO2 beam where the heat seals the cut edge and prevents fraying on open-weave cloth. The same manufacturer producing both platforms means the buyer compares real sample cuts side by side rather than relying on a sales brochure. This cross-method comparison removes the guesswork that leads to a machine sitting idle because it was specified for the wrong process [NEED_CITE: comparative sample cutting protocols for knife and laser systems].
Reading the Specs That Actually Matter in Production
The 1600 × 2500 mm working area sets the maximum single-sheet footprint, but the real constraint is how the vacuum table holds material across that area. A flat working table with a 7.5 kW vacuum pump must zone its suction to grip small nested parts without pulling excess air through empty zones — a detail that only matters once the nesting software starts laying out patterns. The Swiss imported knife with vibration full and half cutting modes controls depth by oscillation frequency rather than static pressure, which keeps layered fabric from shifting between plies. Repeated accuracy of ≤0.1 mm, maintained by Yaskawa servo motors and Hiwin linear guides, determines whether pattern pieces from the first sheet and the hundredth sheet still align during sewing [NEED_CITE: servo and linear guide influence on repeated positioning accuracy in CNC cutting].
The Hidden Cost of Skipping Configuration Checks
A buyer who confirms working area but skips tool head selection often discovers the problem on day one of production. The oscillating knife struggles against dense composite layers it was never configured to penetrate, or the vacuum zoning leaves small gasket parts lifting off the table mid-cut. Operators compensate by slowing the feed rate, which silently erodes daily throughput. In worst cases, the material delaminates and the batch is scrapped before the root cause is traced back to configuration [NEED_CITE: material delamination causes in CNC flatbed cutting].
Why Buyers Source This Range Here
In-house design covers both knife and laser platforms, so the recommendation starts with the buyer’s material rather than the factory’s preferred machine. Tool head and table configuration are specified per material type and production volume before the order is finalised. Software compatibility — including HP-GL file import and nesting workflows — is confirmed during the quotation stage, not after delivery. Voltage, plug type and control panel language are matched to the destination market. Sample cutting on the buyer’s own material runs before commitment, so the cut edge, not the brochure, makes the decision.
Documentation & Verification
- Machine specification sheet listing tool head and vacuum table configuration for your material
- Electrical schematic confirming voltage and frequency for your local supply
- Sample cutting report produced on your fabric or composite before order confirmation
- HP-GL format compatibility note matched to your existing nesting software
- Factory test record documenting repeated accuracy across the full working area
- Packing photographs showing machine secured for ocean freight
Installation, Commissioning & Support
- Floor space of approximately 3450 × 2300 mm plus operator clearance required for the RT-D2516/RT-S2516 footprint
- Dedicated 380V ± 10% circuit with capacity for combined 9 kW machine and 7.5 kW vacuum pump load
- Machine arrives with table and gantry separated; reassembly and levelling performed on site
- First-run calibration of Yaskawa servo axes and vacuum zone mapping before production starts
- Operator training covers HP-GL file import, tool head changeover and blade depth setting
- Spare blade and belt inventory specified based on your material abrasiveness and shift pattern
What We Need From You Before Quoting
Send the exact fabric or composite specification — fibre type, weight per square metre, number of layers and total thickness — along with your largest sheet size and daily cutting volume. Confirm your workshop voltage and frequency, and tell us which nesting or CAD software you currently run so we verify file compatibility before the quotation is issued.
Frequently Asked Questions
Q: Should I choose oscillating knife or laser for my fabric cutting line?
A: Oscillating knife suits layered fabric, foam and composites where heat would melt adhesive layers or leave hard sealed edges. Laser suits single-ply textiles and synthetics where edge sealing prevents fraying. Request sample cuts on your actual material to compare edge quality, then decide based on the result rather than the specification sheet.
Q: How do I select the right tool head for my material thickness?
A: The Swiss imported knife on the RT-D2516/RT-S2516 offers vibration full cutting for complete penetration and half cutting for kiss-cut applications. Provide your material type, total thickness and layer count so the correct blade profile and oscillation frequency are matched before the machine is configured.
Q: Will the vacuum table hold small nested parts during cutting?
A: The flat working table with 7.5 kW vacuum pump must be zoned to maintain suction only under the material footprint. Share your typical nesting layout and smallest part size so the vacuum zoning is configured to prevent part lift without wasting suction on empty table areas.
Q: Can the machine work with my existing nesting software?
A: The instruction system accepts HP-GL compatible format. Before order confirmation we run a file format compatibility check against your nesting software output and provide a written compatibility note, so you know the workflow connects before the machine arrives.
Q: What happens if my local voltage differs from 380V?
A: Voltage is configurable to match your supply. The electrical schematic is confirmed during quotation, and the correct transformer, motor winding and control components are installed at the factory. This verification step prevents motor burnout and control faults after installation.










商品评价
There are no reviews yet.