

Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
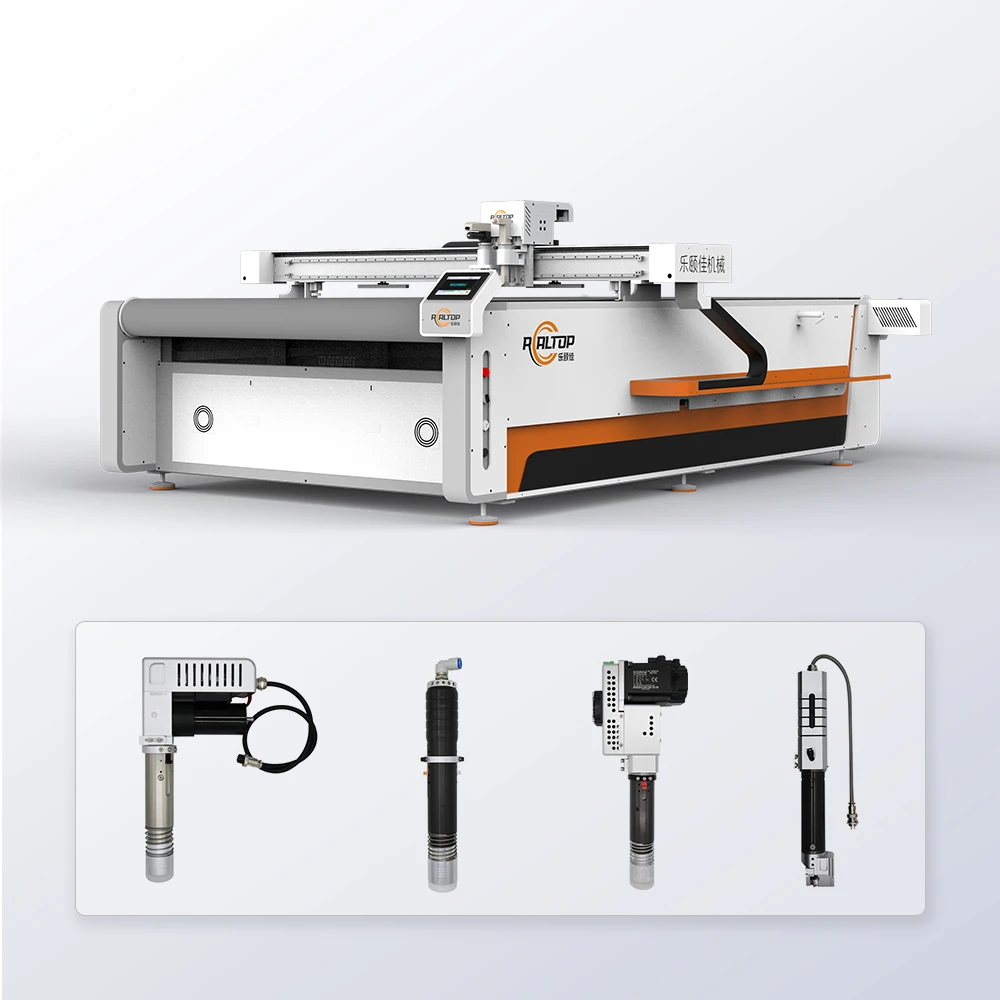
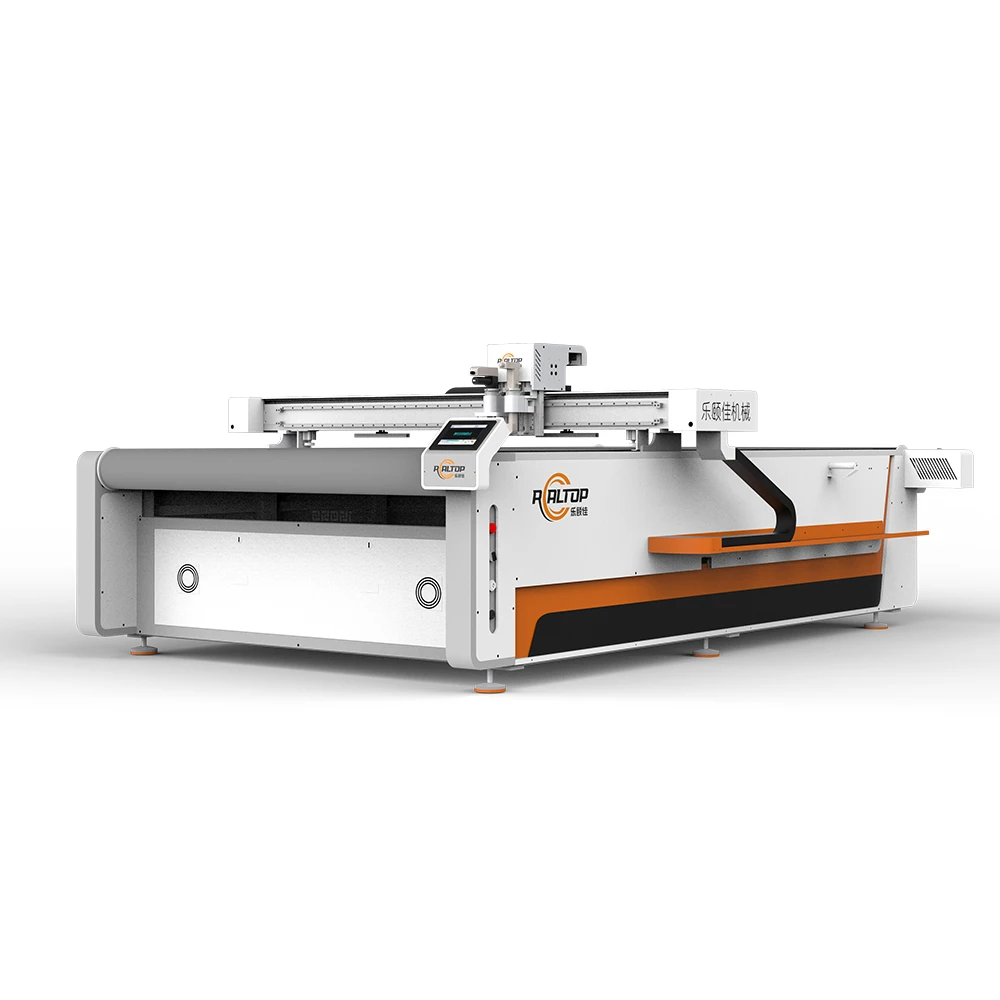
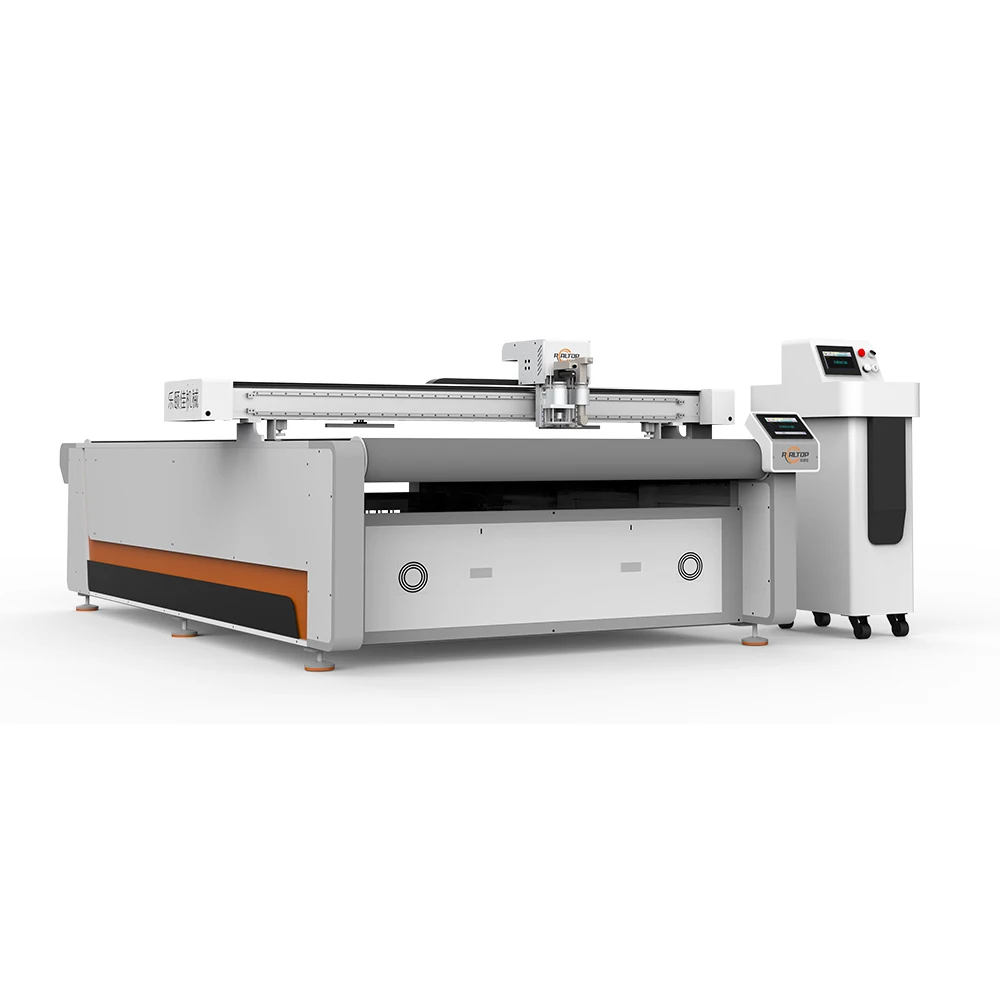
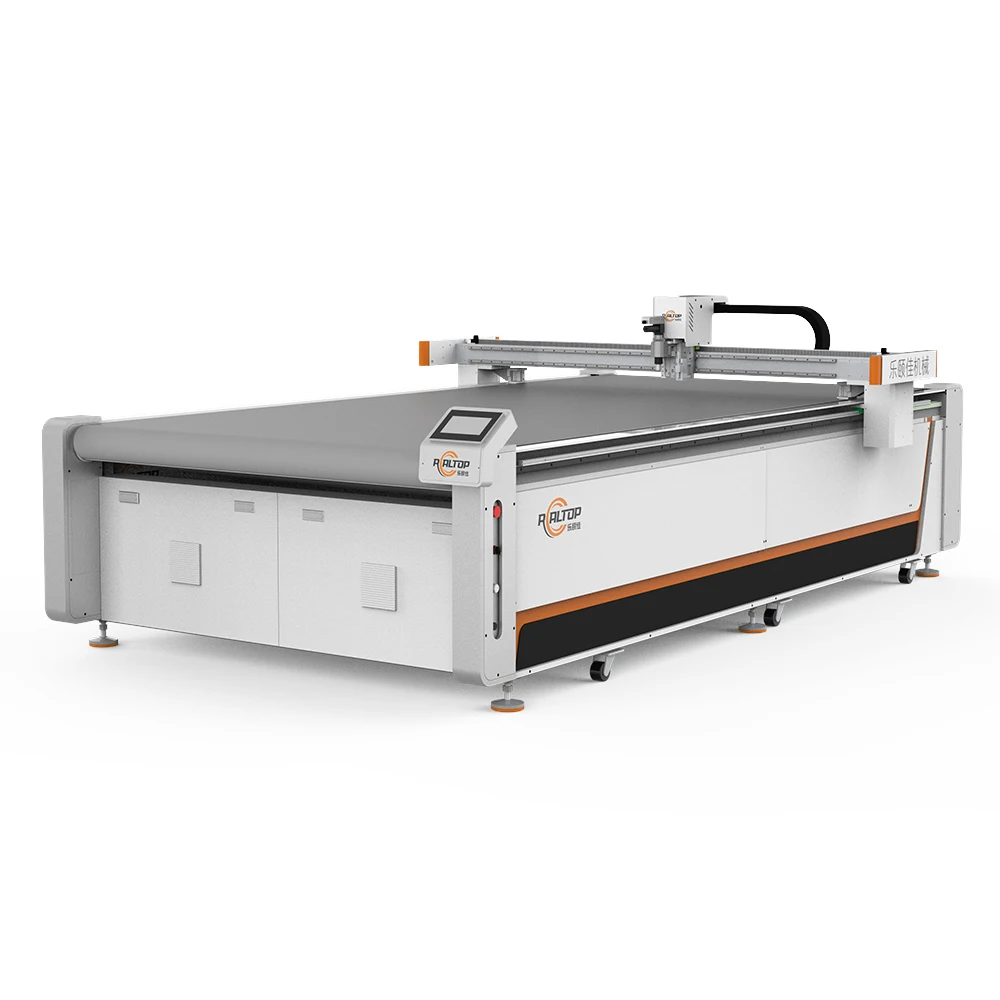
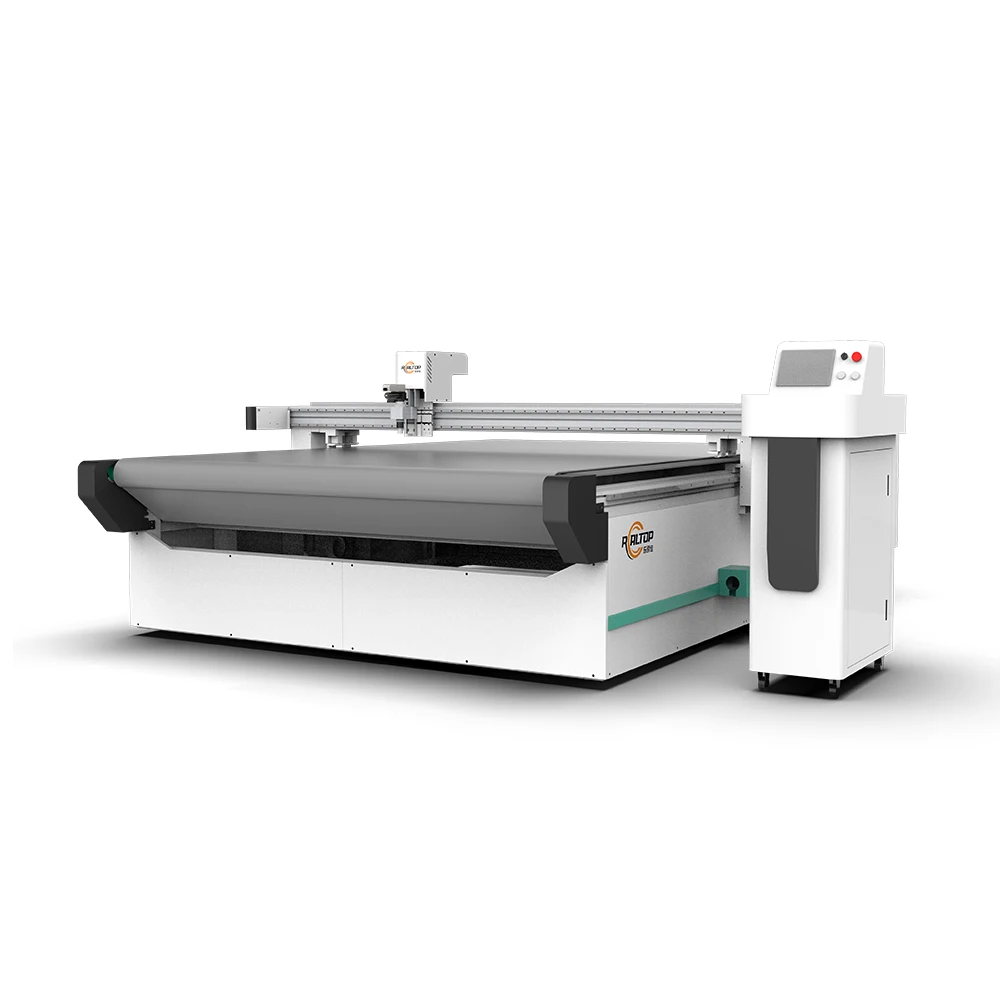
In-House Knife and Laser Design — the 1625 flatbed platform covers oscillating, rotary and kiss cutting under one roof, so fabric converters choose the tool head that matches the material rather than forcing the material to fit the machine.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | 1625 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600 × 2500 mm |
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V groove knife |
| Cutting Speed | 0–2000 mm/s |
| Maximum Cutting Thickness | ≤ 30 mm |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Pump | 9 kW |
| Voltage Options | 110 V / 220 V / 380 V (basis not stated in source — confirm frequency and phase configuration) |
| Profile Formats | PLT, DXF, AI, PDF |
| Control System | PLC control panel |
| Servo Motor Options | Panasonic, Delta, Dorna |
| Vacuum Table | Aluminum bellows vacuum table |
| Safety Devices | Infrared sensor, Emergency stop |
| Machine Size | 3300 × 2100 × 1350 mm |
| Software Language | English, Russian, Italian, Chinese, customizable |
Application Suitability
| Application | Material or Output |
|---|---|
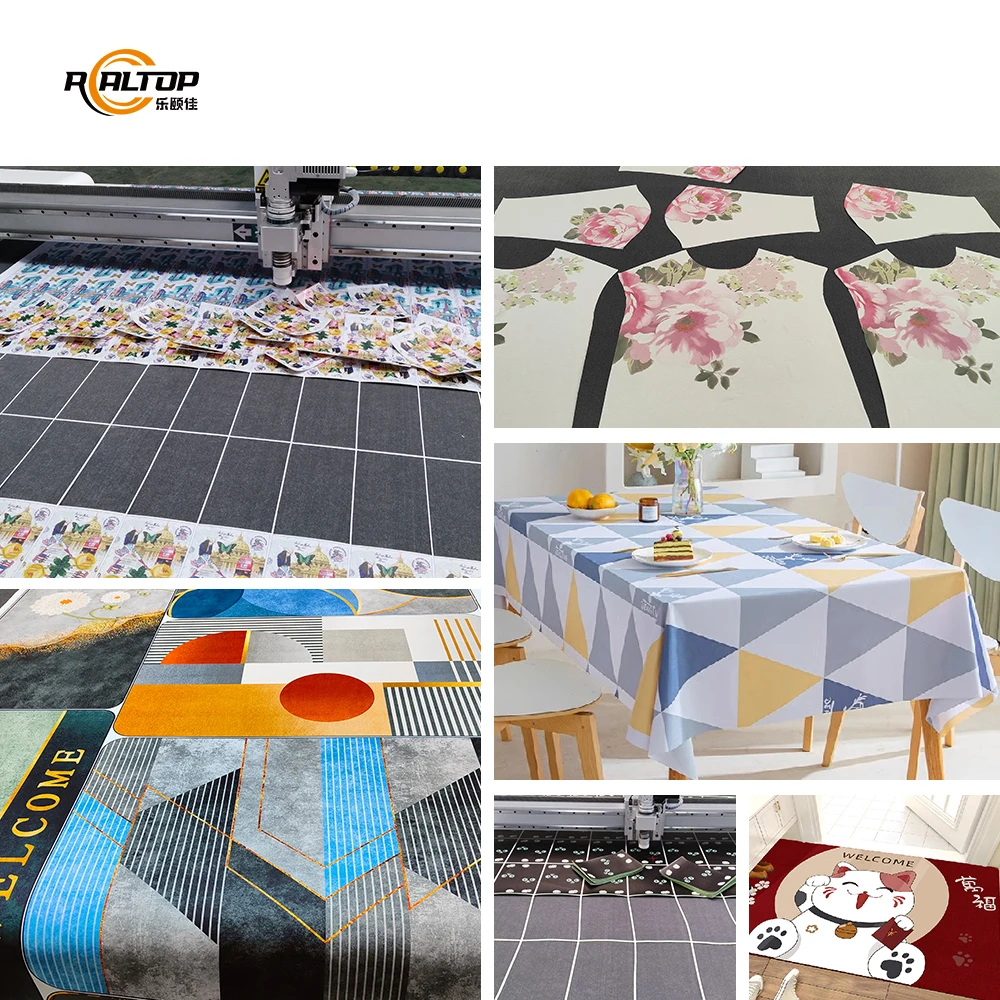
| Apparel manufacturing | Suits, knitwear, lace, complex woven and technical fabrics |
| Automotive interiors | Seat fabrics, carpets, PVC floor mats |
| Home textiles | Sofa upholstery, curtain panels, area rugs |
| Composite processing | Carbon fiber prepreg, aramid fabrics |
| Packaging sample making | Cardboard, corrugated carton, folding box prototypes |
| Advertising and signage | Vinyl, foam board, PVC banner material |
Why "1600 × 2500" Tells You Nothing About the Cut
A working area figure on a nameplate does not tell you whether the knife will shear through four-layer bonded foam or leave ragged edges on lightweight spandex. A CNC oscillating knife cutting machine manufacturer must match the tool head, oscillation frequency and vacuum zoning to the actual material stack before the crate is nailed shut [NEED_CITE: industrial cutting tool head selection by material density].
The cut quality is set in the sample room, not on the spec sheet.
I have watched buyers focus on table size, sign the contract, then discover the standard oscillating blade cannot handle their multi-layer composite layup. Three days of remote parameter tuning later, the real cost of skipping a material trial shows up in missed shipment deadlines. That is why every 1625 leaving the Jinan floor carries a signed sample cutting report run on the buyer’s own roll stock.
Matching the Knife to the Cloth
The 1625 platform supports seven tool head variants, each engineered for a specific failure mode in textile cutting. A driven rotary knife keeps continuous cuts on knits free of fraying, while a pneumatic knife handles the crush-sensitivity of open-cell foams that would otherwise flatten under a standard oscillating blade. Selecting the wrong head does not just produce a poor edge; it alters the nesting yield because operators leave wider kerf margins to compensate for drag.
Contour Recognition Without the Guesswork
Printed sublimation fabrics demand CCD camera positioning that can track registration marks at full traverse speed. If the vision system is rated only for slow jog feeds, the production nest runs at a fraction of the nominal 2000 mm/s cutting speed [NEED_CITE: CCD registration accuracy at production feed rates]. The 1625 accommodates camera modules calibrated for high-contrast dye-sub marks, keeping contour accuracy within the ±0.1 mm tolerance even on multi-color printed panels.
Reading the Spec Sheet Between the Lines
The 9 kW vacuum pump paired with an aluminum bellows table is sized for high-permeability fabrics where air leaks through the weave. Zoning the table into independent sectors prevents small pattern pieces from lifting once the main vacuum area is uncovered by nested parts. Meanwhile, the ±0.1 mm accuracy figure assumes a flat bed; warped MDF spoil boards or worn conveyor belts introduce cumulative drift that no servo can correct. Specifying a replaceable cutting mat on top of the aluminum surface extends the interval between accuracy recalibrations.
Servo choice — Panasonic, Delta or Dorna — affects low-speed torque delivery during tight-radius cuts on heavy canvas. A servo that hunts at 50 mm/s will leave micro-steps visible on curved seam allowances.
The Price of a Missed Configuration Check
When voltage arrives at the wrong frequency, the 9 kW vacuum pump spins but delivers reduced suction, and small fabric pieces drift during high-speed cornering. Operators blame the blade, swap to a sharper grade, and still see lift marks. The root cause is a 50 Hz pump running on a 60 Hz supply — a detail confirmed in five minutes on the electrical schematic, yet often skipped until the machine is bolted to the floor [NEED_CITE: frequency mismatch effects on centrifugal vacuum pumps].
Why Buyers Route Fabric Orders Through Jinan
- Dual-technology design office — knife and laser cutting paths are compared in-house so the 1625 is specified only when a blade genuinely outperforms a CO2 beam on the buyer’s material.
- Pre-shipment sample cutting — the buyer’s fabric roll is run on the exact 1625 configuration, and a signed cutting report ships with the machine.
- File format compatibility audit — PLT, DXF, AI and PDF nesting files are test-processed before order confirmation, avoiding software dead-ends on the production floor.
- Voltage and language lock-down — the PLC panel language and power configuration are frozen on the purchase order, not guessed at the packing stage.
- CE-marked electrical build — documentation package includes a declaration aligned to the machinery directive, easing customs clearance in regulated markets.
Documentation & Verification
- Machine specification sheet listing every tool head option and table zone
- Electrical schematic confirming voltage, phase and frequency for destination market
- Factory test record cut on buyer’s fabric roll before crating
- Software licence and nesting file format compatibility note
- CE declaration covering mechanical and low-voltage directives
- Spare parts list with oscillating blade and cutting mat reorder codes
Installation, Commissioning & Support
- Level the 3300 × 2100 × 1350 mm frame on a flat concrete slab; allow clearance for full 2500 mm Y-axis travel.
- Feed the 9 kW vacuum pump from a dedicated 380 V three-phase breaker; avoid shared circuits with welding loads.
- Confirm PLC control panel language matches operator proficiency before first power-on.
- Calibrate vacuum table zoning with the buyer’s smallest nested pattern piece to verify hold-down.
- Train operators on tool head changeover between oscillating, rotary and kiss cutting tools.
- Stock replacement oscillating blades and aluminum bellows seals for typical six-month consumable intervals.
Before You Request a Quote
Send a representative fabric swatch with layer count and daily yardage target. Confirm your facility voltage and frequency so the pump and servo drives are wound correctly. If you run an existing nesting workflow, share a sample file so we can verify profile import before the build starts.
Frequently Asked Questions
Q: How do I decide between an oscillating knife and a CO2 laser for my fabric?
A: Knives excel on multi-layer layups and materials where a heat-sealed edge is undesirable, such as natural fibers destined for dyeing. Lasers seal synthetic edges and handle intricate lace patterns without blade drag. We run both methods on your sample swatch and report edge quality, kerf width and cycle time before you commit to one configuration.
Q: Which tool head should I specify for cutting automotive seat foam?
A: Open-cell foams typically require a pneumatic knife to prevent crushing at the cut entry point. The 1625 platform lets you swap to an oscillating knife for the vinyl cover layer on the same table, so both operations run without moving the blank between machines.
Q: Will the CCD camera track printed marks on high-speed dye-sub fabric?
A: The camera module is calibrated for high-contrast registration marks at production traverse speeds. We verify tracking accuracy on your printed roll during the pre-shipment sample run, and the signed report accompanies the machine so you know the ±0.1 mm tolerance holds on your specific ink and substrate combination.
Q: What if my nesting software outputs a format not listed on the spec sheet?
A: We test your actual nesting files — PLT, DXF, AI or PDF — through the 1625 control software before order confirmation. If a custom post-processor is needed, the requirement is captured on the purchase order, not discovered on your first production day.
Q: How does vacuum table zoning affect small garment pattern pieces?
A: Small pieces lose hold-down once surrounding material is cut away. The aluminum bellows table on the 1625 divides into independently valved sectors so suction concentrates where parts remain. We zone the table layout to match your nesting software’s part sequence during the factory test.










商品评价
There are no reviews yet.