
Fast Delivery
Quick, reliable shipping to any location.

Free & easy returns
Return this item by mail or in store within 90 days for a full refund.
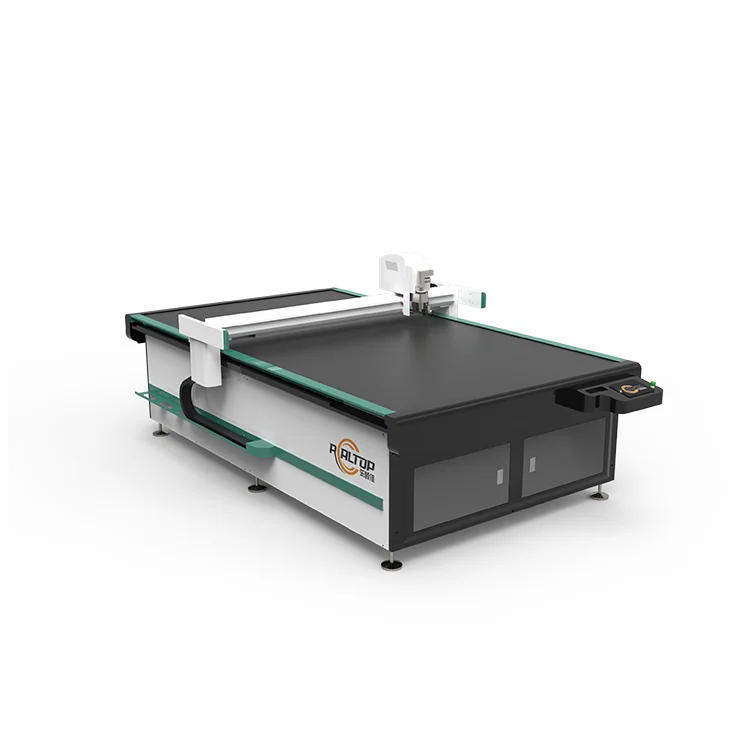
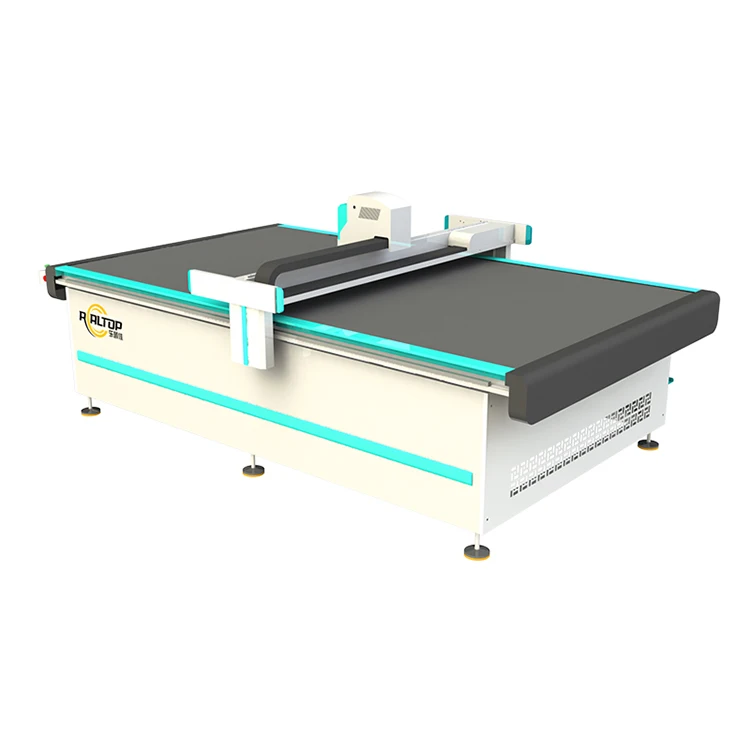
Complete Cutting Catalogue Approach — A buyer surveying both knife and laser options can map this 1600×2500 mm CNC oscillating knife cutting machine for sale against the full REALTOP range, matching the cutting method to the material rather than forcing one technology across every job.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516 / RT-S2516 |
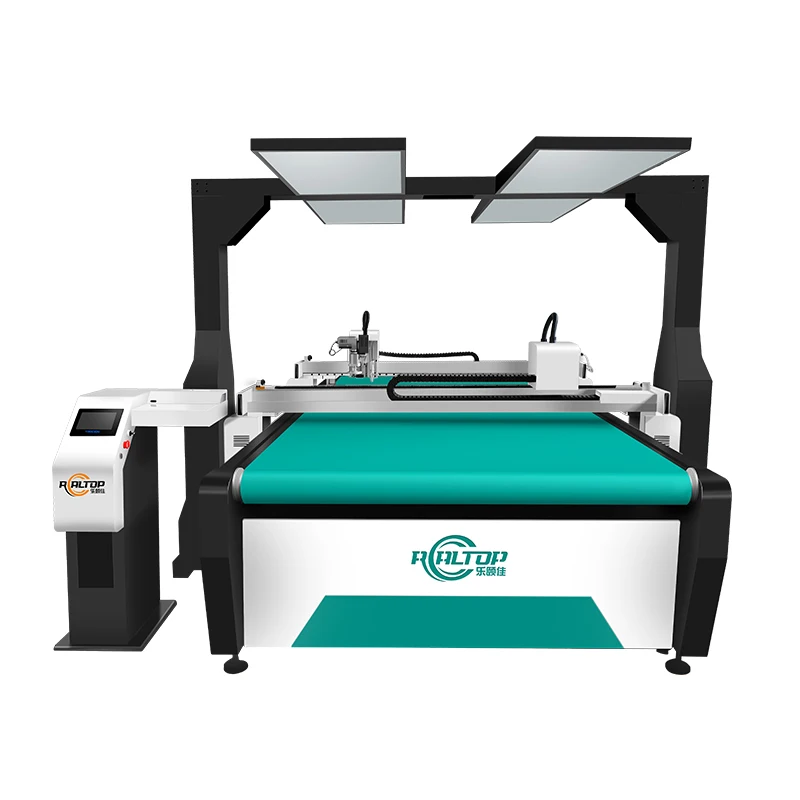
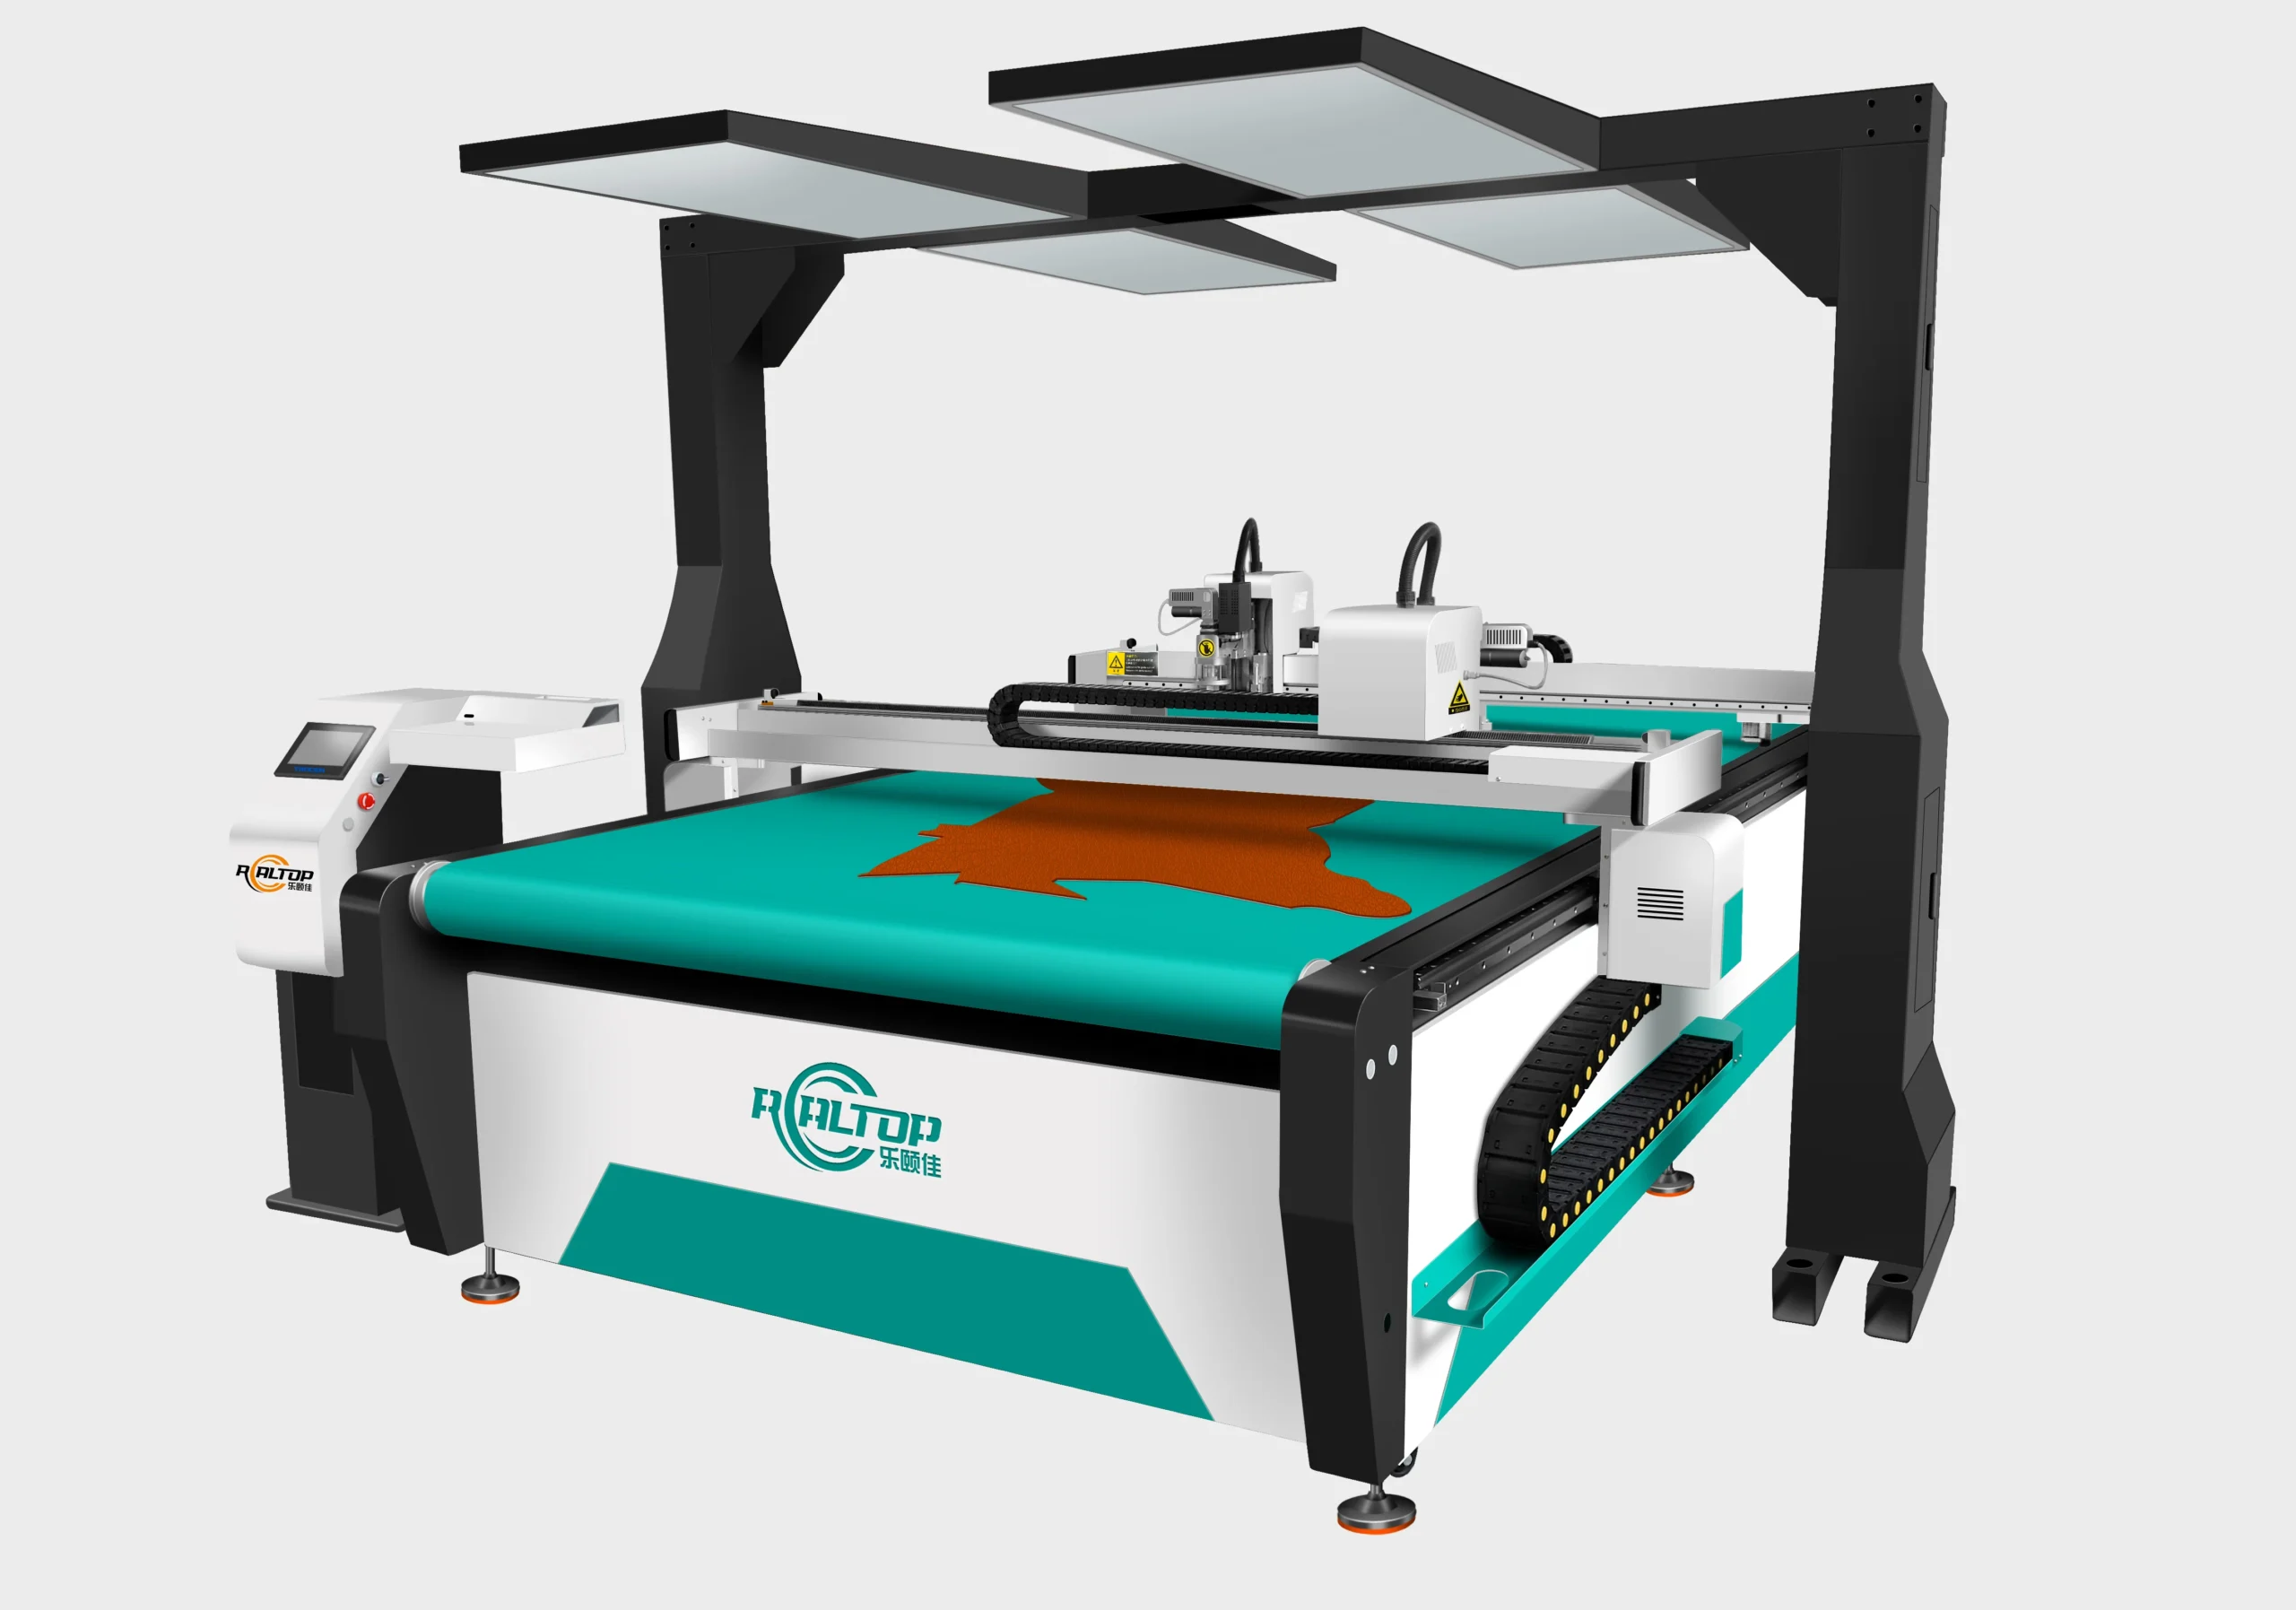
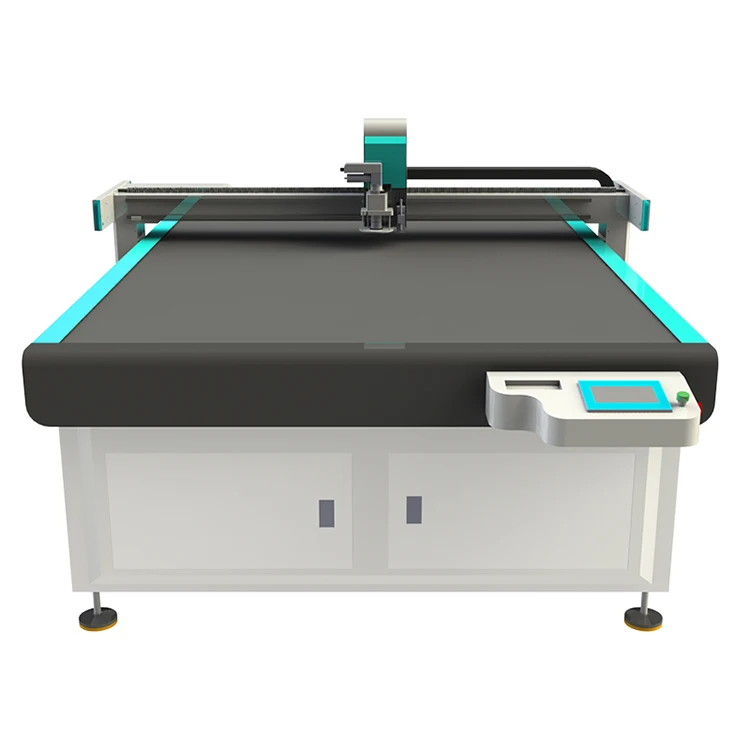
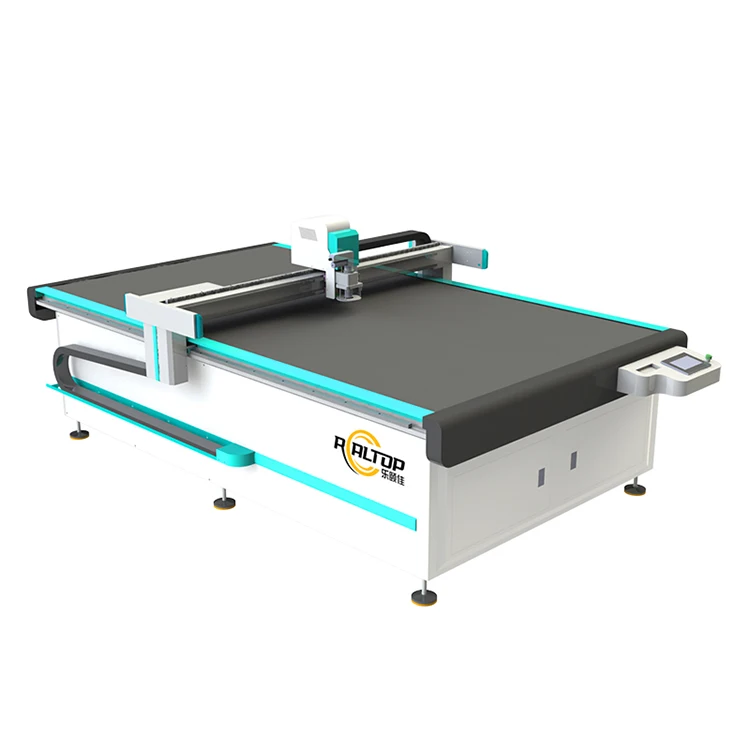
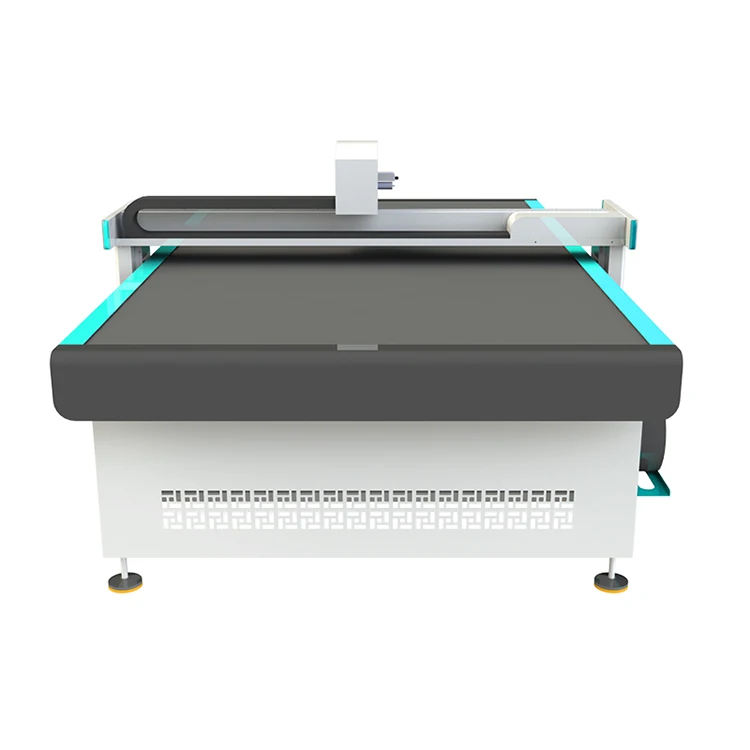
| Product Type | CNC Oscillating Knife Cutting Machine with Vision System |
| Working Area | 1600 × 2500 mm |
| Machine Dimensions | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Voltage | 380V ±10% (50Hz/60Hz to be confirmed) |
| Control System | CNC with HP-GL compatible format |
| Servo Motor | Delta digital servo |
| Linear Guide | Taiwan Hiwin rail |
| Transmission | Synchronous belt and ball screw |
| Translational Velocity | 800–1200 mm/s |
| Cutting Thickness | 20–80 mm (basis not stated in source — verify against material type and density) |
| Repeatability | ≤0.1 mm |
| Positioning Accuracy | ±0.1 mm |
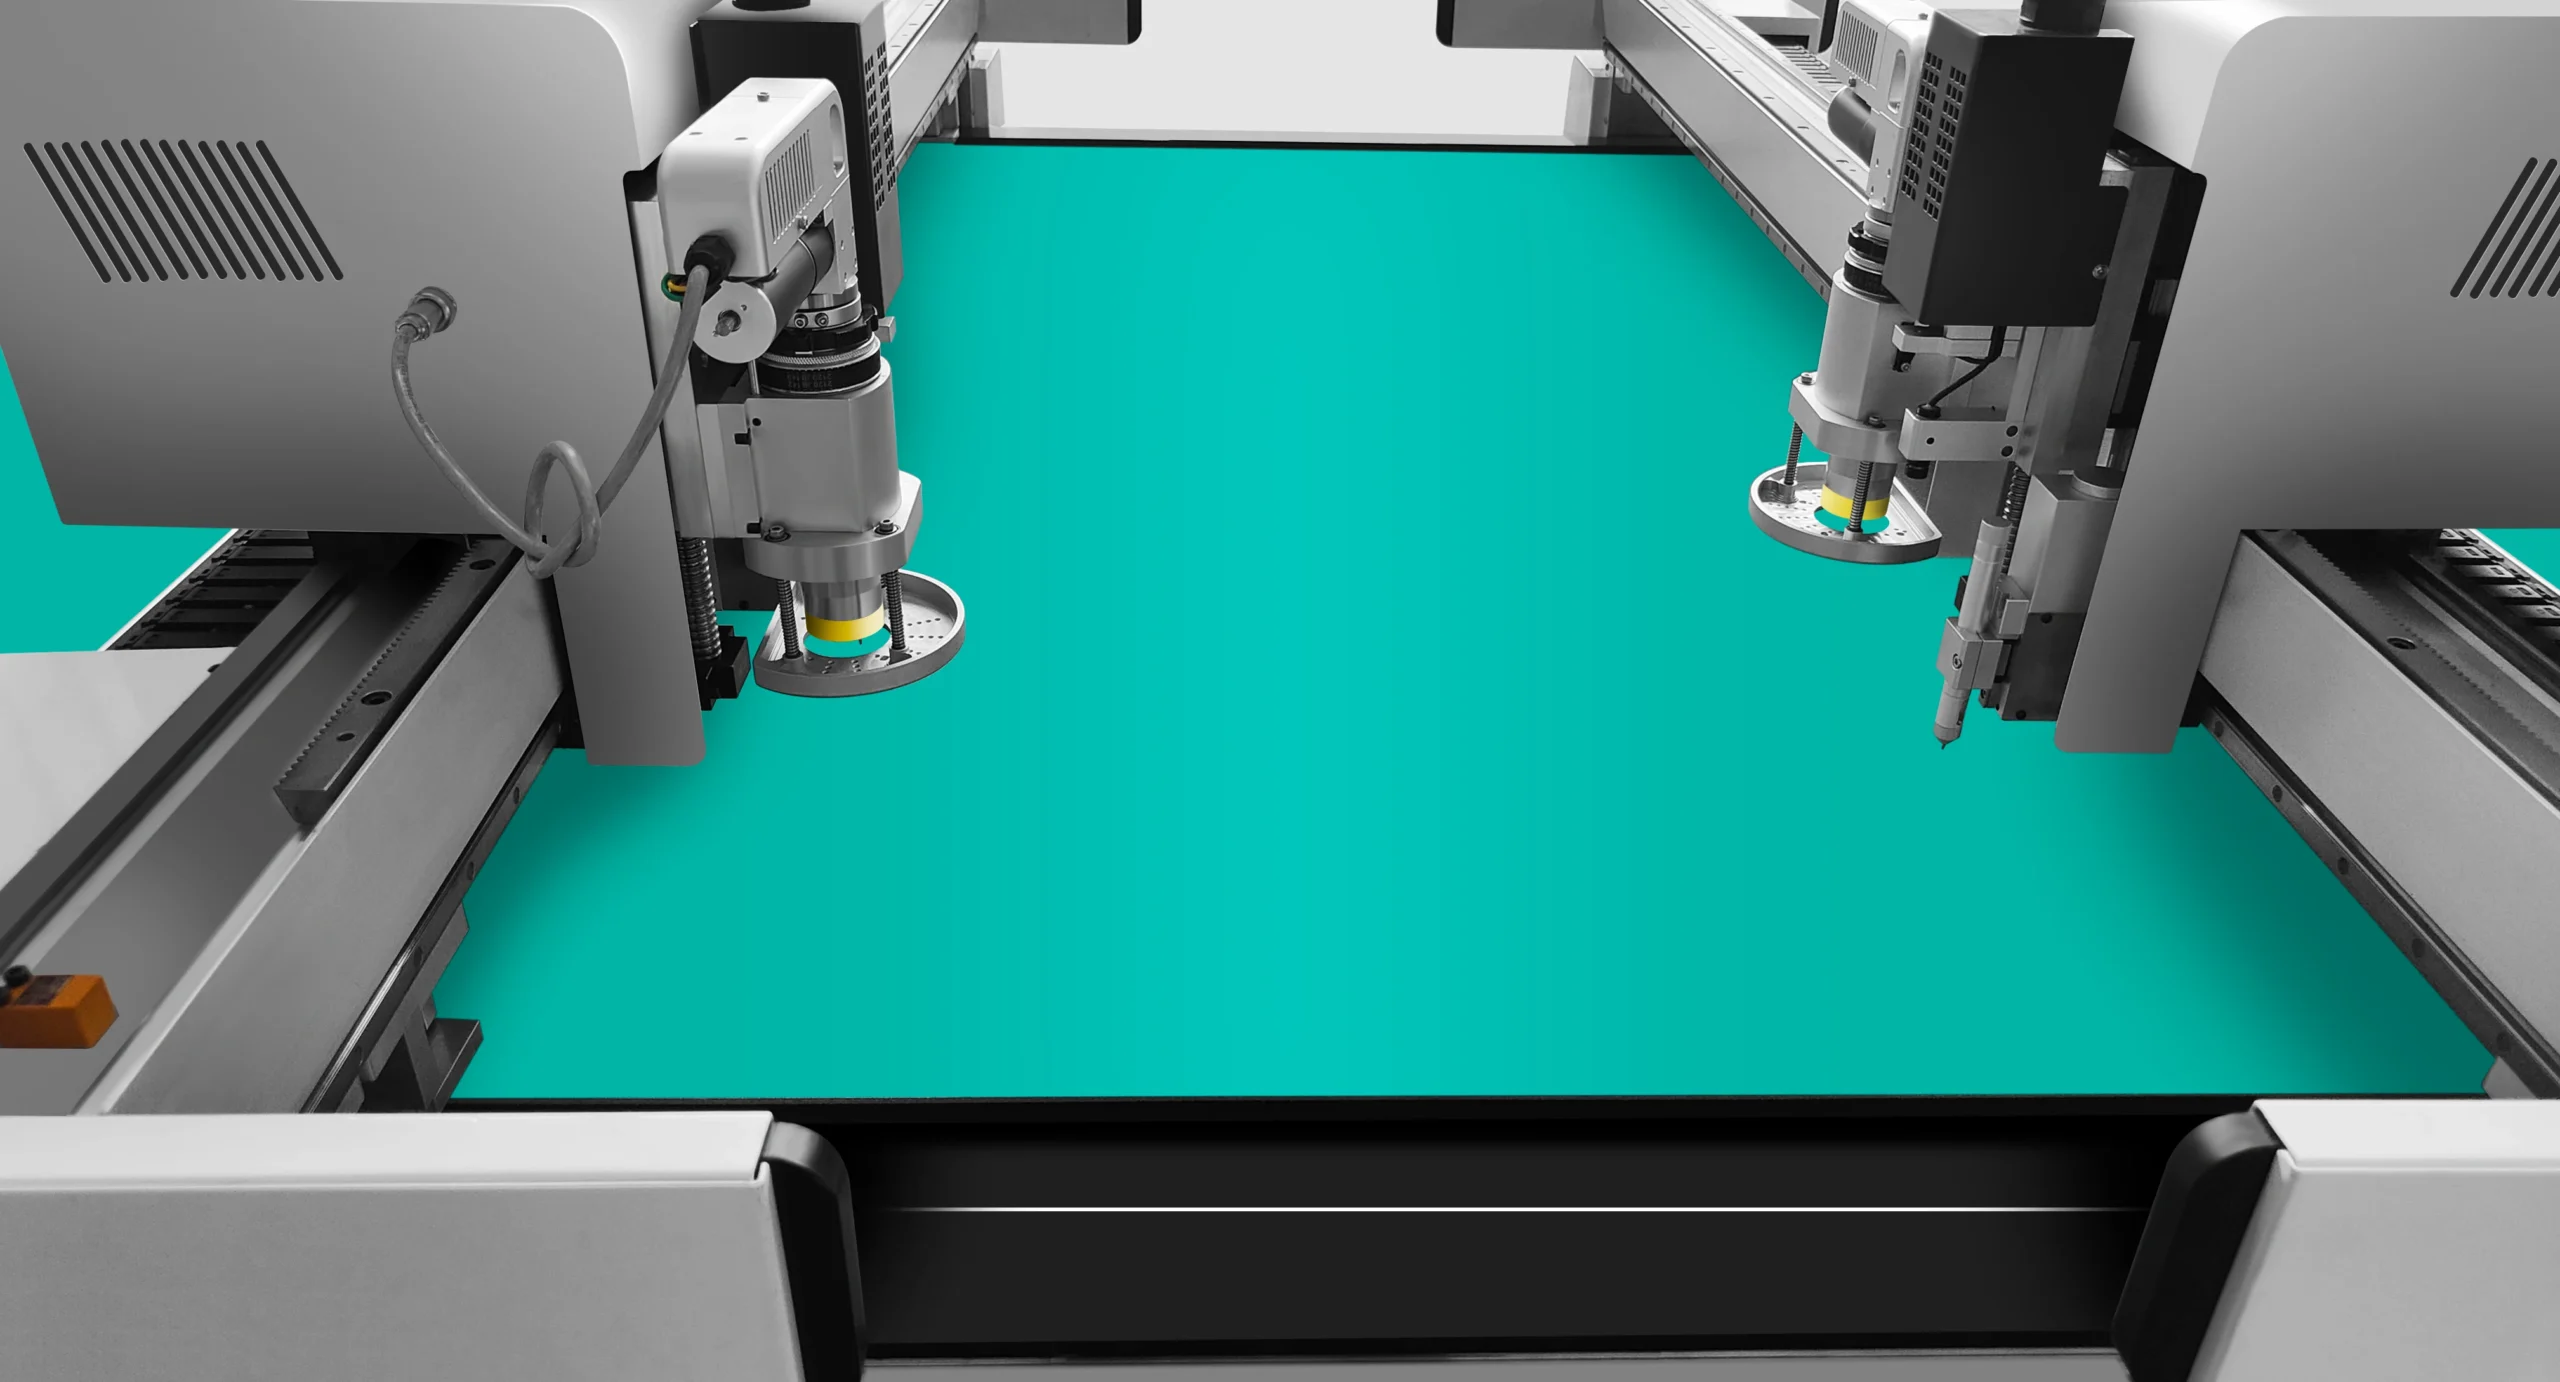
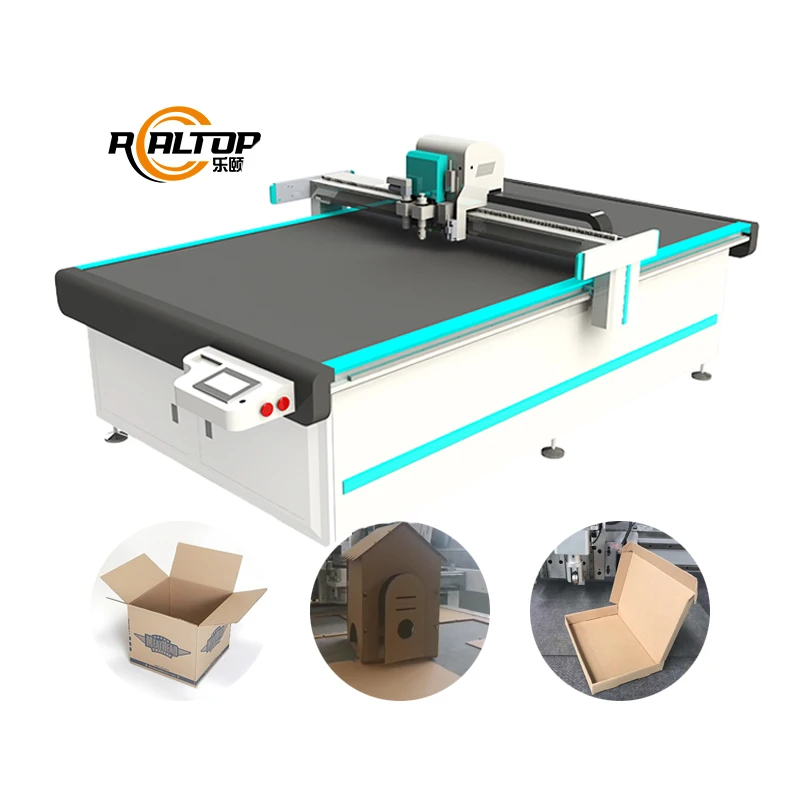
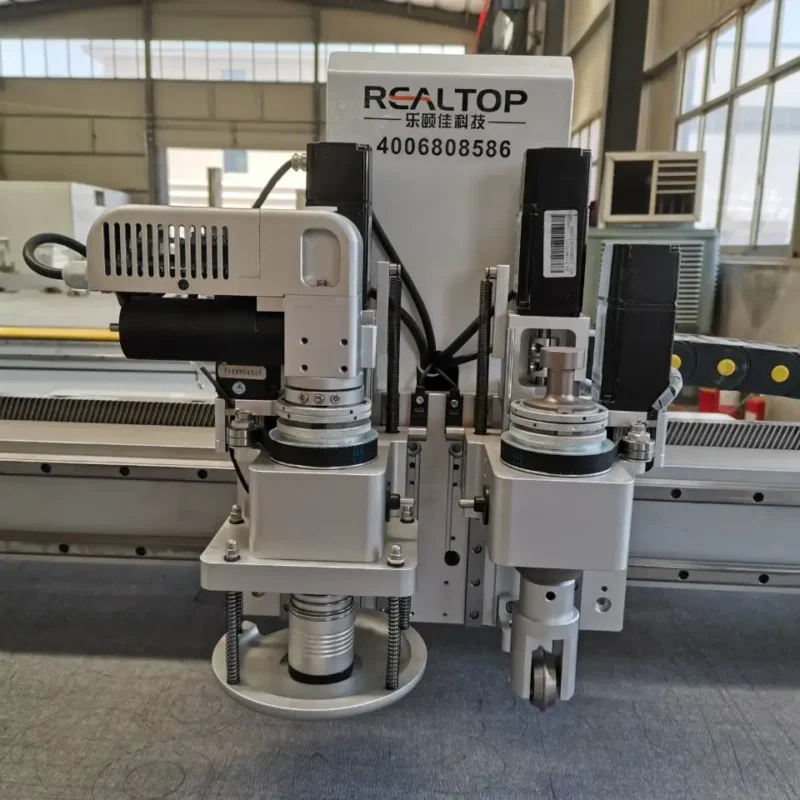
| Tool Head | Multifunctional: oscillating knife, drag knife, creasing wheel, punching, marking, CCD |
| Vision System | Small CCD mark point positioning; panoramic camera recognition; optional projection positioning |
| Working Table | Flat vacuum table with aluminum alloy adsorption |
| Vacuum Pump | 7.5 kW |
| Conveyor Belt | Germany imported, auto feeding and receiving |
| Safety Device | Infrared sensors |
| Software | Self-developed nesting and pattern design; multi-language interface |
| Patents | 5 patents technology certification (domestic and international) |
Application Suitability
| Application | Material or Output |
|---|---|
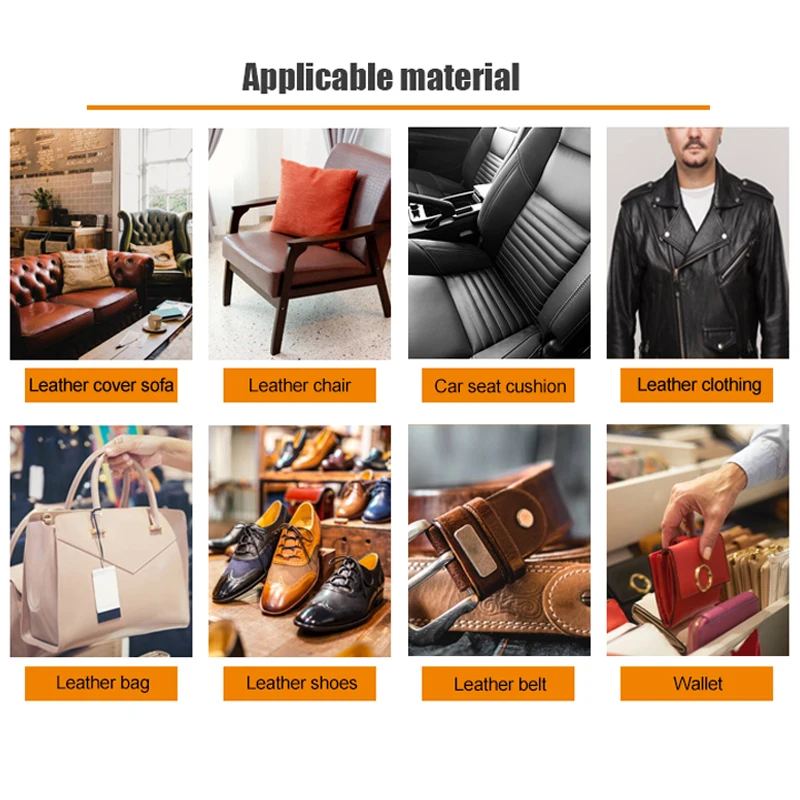
| Automotive interior trimming | Leather, synthetic leather, PU, EVA, XPE foam for seat covers and floor mats |
| Garment and footwear production | Woven fabric, non-woven textile, shoe uppers, luggage material |
| Gasket and sealing fabrication | Rubber, PTFE, ETFE, composite sealing sheets |
| Packaging and carton sampling | Corrugated cardboard, plastic box stock, sticker film |
| Soft furnishing and carpet | Carpet rolls, sponge, foam board, cloth for upholstery |
When "20–80 mm Cutting Range" Means Different Things on Different Materials
A CNC knife cutting machine for sale with a stated thickness range only tells half the story — material density, layer count, and tool head choice determine whether that range actually applies to your production.
Buyers often see a thickness number on a spec sheet and assume it covers everything they plan to run. The reality on the shop floor is that cutting 80 mm of low-density sponge is a completely different operation from cutting 20 mm of compressed fiberglass laminate. When the material does not match the assumption behind the number, the knife either fails to penetrate or drags the layers apart, leaving ragged edges that have to be reworked by hand [NEED_CITE: oscillating knife cutting behavior across material densities]. The cost shows up not as a machine failure but as scrap rate and operator frustration.
Knife Versus Laser: Picking the Right Method for the Material
This is the first question a buyer surveying a full cutting catalogue needs to answer. Oscillating knife technology cuts by physical blade vibration, which works well on layered fabric, thick foam, leather, and rubber gasket material where a laser would melt, burn, or leave hardened edges. The multifunctional tool head on the RT-D2516 / RT-S2516 lets a single setup switch between a vibrating knife for full-depth cuts and a creasing wheel for fold lines on carton samples, keeping the operator at one machine rather than moving jobs between stations.
Panoramic Vision and the Limits of Mark Point Tracking
The panoramic camera recognition system and small CCD mark point positioning are designed to locate printed contours on materials like advertising vinyl or pre-printed fabric. For a CNC knife cutting machine for sale with vision, the critical variable is whether the camera can actually read the marks on your specific material at production speed. Dark marks on light fabric track reliably; low-contrast marks on textured leather or heavily grained surfaces can cause the system to lose registration mid-sheet [NEED_CITE: CCD vision positioning accuracy on textured surfaces]. This is why a sample cutting test on the buyer’s actual material is the only meaningful verification before commitment.
Reading the Specs That Matter on the Floor
The Delta servo motor paired with Taiwan Hiwin linear guides delivers ±0.1 mm positioning accuracy across the full 1600 × 2500 mm working area. In practice, this tolerance matters most when cutting interlocking pattern pieces for automotive seat covers or shoe uppers, where even a small drift over a long cut path accumulates into misalignment at assembly. The 7.5 kW vacuum pump and aluminum alloy flat table hold material in place during cutting, but vacuum zoning effectiveness depends on part size — very small pieces can still lift if the suction zones are not matched to the nesting layout. The HP-GL compatible control system and self-developed nesting software handle file import, but buyers need to confirm that their existing design files and nesting workflows integrate before the machine ships. Translational velocity of 800–1200 mm/s applies to travel moves, not cutting speed, which varies significantly with material thickness and tool head selection.
What Happens When the Wrong Tool Head Meets Your Material
Choosing an incorrect tool head for the material produces problems that do not show up until production starts. A drag knife meant for thin vinyl will crush and tear when pushed through 40 mm foam, generating debris that contaminates the vacuum table. An oscillating knife set to the wrong vibration frequency on layered composite material can delaminate the top layers before the cut is complete. These failures look like material defects to the operator, but the root cause is a configuration mismatch that should have been caught during sample testing [NEED_CITE: tool head selection impact on edge quality in CNC knife cutting].
Why Buyers Source the Full Range Here
In-house design and production cover both knife and laser cutting technologies, so a buyer comparing methods gets an honest recommendation based on the material rather than being steered toward whichever machine is in stock. Tool head and table configurations are specified per material and production volume, not sold as a one-size package. CCD camera positioning capability is verified against the buyer’s printed material before the order is finalized. Software compatibility — file format import, nesting workflow, and control language — is confirmed in documentation before shipment. Sample cutting on the buyer’s own material provides a physical report that both sides can evaluate before commitment.
Documentation & Verification
- Machine specification sheet covering RT-D2516 / RT-S2516 full configuration and optional vision modules
- Electrical schematic with 380V ±10% voltage and frequency confirmation for target market
- Tool head and vacuum table configuration list matched to your material type
- Sample cutting report produced on your actual material with edge quality documentation
- Software licence and file format compatibility note confirming HP-GL import and nesting fit
Installation, Commissioning & Support
- Floor space planning for 3450 × 2300 × 1250 mm machine footprint with conveyor clearance
- Dedicated 380V circuit with confirmed 50Hz or 60Hz frequency for servo and vacuum pump
- Fully assembled delivery with vacuum table leveling and belt tension check on site
- First-run parameter tuning for oscillation frequency and vacuum zoning on your material
- Operator training on multifunctional tool head changeover and panoramic camera calibration
- Spare parts list covering Swiss knife blades, CCD calibration targets, and belt segments
What to Include in Your Inquiry
To get a configuration that actually fits your production line, provide the material type, thickness, and maximum sheet size you plan to cut. Specify your daily volume so the nesting software and auto-feeding setup can be matched to your throughput requirements. Confirm the local voltage and frequency at your facility, along with the preferred control language for the operator interface [NEED_CITE: voltage and frequency standards by export market].
Frequently Asked Questions
Q: How do I verify the 20–80 mm cutting thickness claim for my specific material?
A: The stated range depends on material density and composition, not just thickness. We run a sample cutting test on your actual material and provide a report showing edge quality, tool head used, and achievable speed. This confirms whether the RT-D2516 / RT-S2516 handles your specific stock before you commit to an order.
Q: Which cutting method — knife or laser — is right for my material and volume?
A: Knife cutting suits layered fabric, thick foam, leather, and gasket rubber where laser heat would melt or harden edges. Laser is better for thin synthetics needing sealed edges or detailed engraving. As part of the full REALTOP catalogue, we help you compare both methods against your actual material and daily volume.
Q: Can the panoramic vision system track marks on textured leather at production speed?
A: Mark tracking depends on contrast between the printed mark and the material surface. High-contrast marks on smooth fabric track reliably, but deep-grain leather or low-contrast prints can cause registration loss. A sample test with your printed material is the only way to confirm before ordering.
Q: Will my existing design files and nesting workflow work with the included software?
A: The control system accepts HP-GL compatible formats and the self-developed nesting software handles common file types for carton, automotive, and garment patterns. We verify your specific file format and nesting workflow compatibility before shipment and document it in the software licence note.
Q: What voltage, plug type, and language options should I confirm before the machine ships?
A: The standard configuration is 380V ±10%, but frequency (50Hz or 60Hz), plug type, and control interface language must match your facility. These are confirmed in the electrical schematic document before production starts to avoid rewiring or reconfiguration after delivery.
商品评价
There are no reviews yet.